Industry Portal
Related News
- 00
0000-00
Aluminum Price Fluctuations: Fixed vs. Indexed Supply Contracts - 00
0000-00
ECE-Compliant Lighting for Commercial Vehicles: Approval and Installation Checks - 00
0000-00
Laser Adaptive Headlights: What to Check for Range and Glare Control - 00
0000-00
Precision Forging for Aluminum Wheels: Alloy Selection and Fatigue Performance - 00
0000-00
NEV Industry Standards in China: Which Battery Safety Tests Are Required?
An automotive supplier assessment that reveals quality-system risk
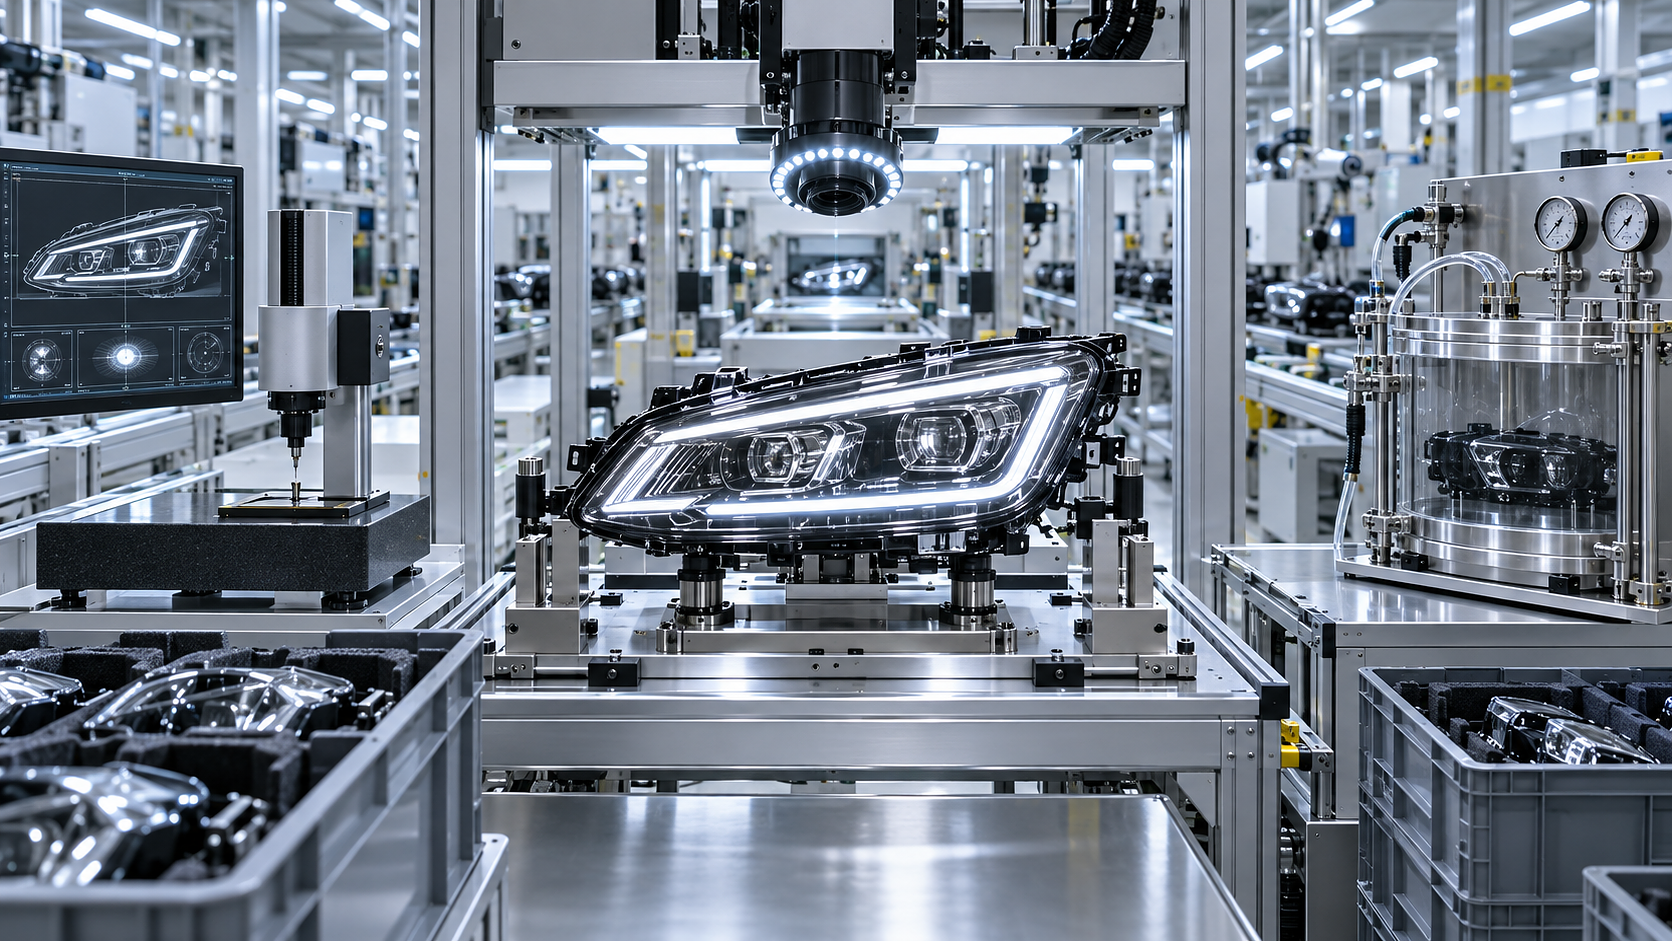
On a supplier’s production floor, risk rarely announces itself as a failed audit or a visible defect. It may appear as a calibration sticker nearing expiry, a temporary work instruction that never made it into controlled documentation, a sub-tier resin source changed without a formal review, or a headlamp validation report that cannot be traced to the production configuration. By the time a defect reaches a vehicle plant or the field, these small gaps have often connected into a much larger problem.
An automotive supplier assessment is therefore more than a compliance exercise. For quality and safety teams, it is an early-warning method for identifying quality-system risk across exterior, vision, and other vehicle-relevant components. In areas such as electric sunroof systems, aluminum wheels, high-performance tires, LED headlamp assemblies, and sensor switches, the assessment must test whether a supplier can repeatedly control the characteristics that affect safety, regulatory conformity, durability, appearance, and customer trust.
The central question is not simply, “Does this supplier hold a certificate?” It is: Can this organization detect variation, contain it, learn from it, and prove that its controls remain effective when materials, volumes, designs, and regulations change?
Why certificates are only the starting point
IATF 16949 certification, often supported by ISO 9001, remains an important screening requirement in automotive supply chains. It indicates that a supplier has been audited against an established quality management framework. Yet a certificate does not automatically demonstrate that every manufacturing line, plant shift, sub-supplier, or new-product launch is under control.
A meaningful automotive supplier assessment looks beneath the certificate and examines how the quality management system behaves in practice. Are internal audits finding real process weaknesses, or only paperwork inconsistencies? Are corrective actions verified for effectiveness months later? Can operators explain the current control plan, or are they relying on informal knowledge accumulated on the line?
This distinction matters particularly for components where an apparently cosmetic feature carries a functional consequence. A wheel finish issue may conceal inadequate pretreatment that later contributes to corrosion. A sunroof water-leak concern may result from variation in adhesive application, glass geometry, drainage routing, or end-of-line testing. A headlamp condensation complaint may trace back to housing weld integrity, vent design, material handling, or a poorly controlled supplier change. A supplier can appear orderly in a conference room while production evidence tells a more complicated story.
The risk profile changes with the component
Not all parts should be assessed with identical emphasis. A generic audit checklist can miss the failure mechanisms that matter most for exterior and vision systems. The audit scope should reflect the component’s safety relevance, regulatory exposure, manufacturing complexity, and likely field-failure modes.
- Electric sunroof systems: Focus on water management, bonding and sealing process capability, glass handling, anti-pinch performance, motor and rail durability, noise-vibration-harshness controls, and traceability of safety-related electronic parts.
- Aluminum alloy wheels: Review alloy chemistry control, casting or forging parameters, heat treatment, non-destructive testing where applicable, runout measurement, coating adhesion, fatigue validation, and containment for cosmetic versus structural defects.
- High-performance tires: Examine incoming material consistency, compound mixing, tire-building controls, curing parameters, uniformity testing, labeling accuracy, and the supplier’s approach to EV-specific load, torque, rolling-resistance, and noise requirements.
- LED headlamp assemblies: Assess optical aiming and photometric verification, sealing, thermal interfaces, electronic component traceability, software or configuration governance where relevant, and validation against applicable ECE, DOT, or destination-market requirements.
- Auto sensor switches: Pay close attention to functional test coverage, electromagnetic compatibility considerations, environmental robustness, connector integrity, change management, and diagnostic response for sensor-related failures.
The goal is not to turn every assessment into an engineering review of the entire vehicle. It is to identify the few process and system conditions most likely to create an unacceptable defect escape. Quality teams should ask for evidence that links the product’s critical characteristics to the controls used on the shop floor.
Follow the thread from requirement to shipment
One of the strongest ways to conduct an automotive supplier assessment is to select one high-risk characteristic and follow it through the organization. This “vertical trace” often reveals more than a broad review of procedures.
For example, a team reviewing an adaptive LED headlamp may begin with a regulatory or customer requirement for beam performance. From there, the assessment follows the requirement into the design specification, DFMEA and PFMEA, control plan, test methods, operator instructions, gauge calibration, end-of-line records, rework rules, packaging controls, and shipment release. At each step, the assessor looks for continuity.
If the specification calls for a tightly controlled optical parameter, does the process control plan identify it as critical? Is the test equipment capable and maintained? What happens when a result is near a limit? Can the supplier distinguish a true product failure from a measurement-system issue? If a component is reworked, is the product retested using the same acceptance criteria?
A broken thread is often a risk signal. It may indicate that engineering intent has not been translated into manufacturing discipline, or that the documentation is more mature than the process itself.
Five signals that reveal quality-system risk early
1. Process controls that depend on memory
Experienced operators are valuable, but a stable automotive process cannot rely on individual memory to preserve critical settings. Watch for controls described as “the operator knows,” parameter adjustments recorded only in notebooks, or inspection decisions based on an unwritten visual standard. These conditions become especially risky during shift changes, turnover, production ramp-up, and temporary staffing.
Controlled work instructions should be accessible at the point of use, aligned with the current revision, and understandable to the people performing the work. More importantly, observed practice should match the documented process. A flawless procedure in a database does not reduce risk if the live production line follows a different routine.
2. Weak change management
Supplier changes are not limited to major design modifications. A different aluminum source, revised rubber formulation, alternative LED bin, replacement adhesive, new mold cavity, relocated production line, or modified inspection frequency can all affect performance. In NEV programs, where lightweighting, thermal loads, electrical architecture, and aerodynamic targets continue to evolve, “small” changes can have disproportionate effects.
A mature supplier has clear criteria for when customer notification, revalidation, PPAP activity, regulatory review, or additional testing is required. Assessors should verify that recent changes were properly risk-assessed and that the organization can demonstrate implementation discipline. A change log alone is not enough; the question is whether the change reached every affected document, operator, test method, and inventory control point.
3. Traceability that stops at the finished-goods label
Lot identification on a shipping carton is useful, but it may not be sufficient when a concern arises. Effective traceability should make it possible to connect a finished part to relevant production date and shift, material batch, key equipment, process records, inspection results, rework history, and, where appropriate, sub-tier supplier data.
The appropriate depth depends on product risk. For a sensor switch or a headlamp control module, traceability may need to support targeted containment of electronic components and software configurations. For wheels and tires, it should support investigation of material, curing, heat treatment, testing, and production-location variables. Assess traceability through a live exercise rather than a verbal promise: choose a recent lot and ask the supplier to retrieve the full record within an agreed practical timeframe.
4. Corrective actions that close too quickly
Every supplier has nonconformities. The more revealing issue is how it responds when they occur. A weak corrective action often names operator error, provides retraining, and closes the record. A stronger response asks why the system allowed the error to pass through: Was the instruction unclear? Was the fixture capable? Did the detection method lack sensitivity? Was a production target creating pressure to bypass a control?
Look for structured root-cause analysis, containment that protects current shipments, actions addressing systemic causes, and evidence that the action worked over time. Recurring defects under different labels are a warning that the organization is treating symptoms rather than mechanisms.
5. Validation evidence disconnected from production reality
Component validation can look convincing while the production process remains fragile. Prototype-level testing, hand-built samples, or laboratory-controlled conditions may not represent serial production. This is particularly relevant to water ingress, thermal cycling, optical performance, wheel fatigue, tire uniformity, and sensor robustness.
Ask whether validation samples were built using intended production tooling, materials, process settings, and assembly conditions. If the process changed after validation, what triggered reassessment? The relationship between design validation, production validation, and ongoing conformity should be visible—not assumed.
Regulatory readiness should be tested as a living capability
For globally supplied exterior and vision components, compliance is not a static file stored in a quality office. Requirements may vary across ECE, DOT, local lighting rules, chemical restrictions, labeling obligations, and market-specific documentation practices. A supplier assessment should examine who monitors these changes, how impact is evaluated, and how affected products are controlled.
Headlamp suppliers may need disciplined management of optical and functional conformity. Tire and wheel manufacturers must understand marking, performance, material, and market-access implications. Suppliers of roof systems and electronic switches may face overlapping safety, environmental, and vehicle-integration requirements. The relevant standards differ, but the management challenge is similar: regulatory intelligence must reach engineering, purchasing, manufacturing, and quality before nonconforming product reaches a border, an OEM plant, or a consumer vehicle.
For quality leaders, this is also where sector intelligence becomes useful. Monitoring raw-material changes in aluminum and rubber, shifts in NEV platform requirements, evolving lighting architectures, and aftermarket demand can reveal where supplier pressure may emerge. Commercial pressure does not automatically create quality risk, but it can expose weak governance around sourcing substitutions, capacity expansion, or expedited launches.
How to score the assessment without hiding the real story
Numerical scoring can help compare suppliers, prioritize follow-up, and communicate risk to sourcing or program teams. However, a single overall score can create false comfort. A supplier with generally sound systems may still have an unacceptable gap in a safety-critical process; another may have several administrative findings but robust control of critical characteristics.
A practical assessment report separates findings into categories such as:
- systemic quality-management weaknesses;
- product or safety-critical control gaps;
- regulatory and certification exposure;
- traceability and containment limitations;
- capacity, launch, or supplier-change risks; and
- opportunities for process maturation that do not require immediate containment.
Each finding should state the observed condition, the potential consequence, the evidence reviewed, the required action, ownership, and a due date proportionate to risk. Vague wording such as “improve control” invites vague responses. A useful finding makes clear what must be verified: for example, whether a revised control plan includes a defined reaction plan, whether gauge capability is demonstrated, or whether all open inventory is traceable to material lot.
Questions worth asking during the closing meeting
The closing meeting should not be a ritual in which findings are read aloud and accepted politely. It is a chance to test leadership awareness and the supplier’s ability to act under pressure. Ask which process failure worries the plant most, what its most recent customer escape taught it, where sub-tier dependency is highest, and which upcoming change could challenge product conformity.
Listen for specificity. Leaders who understand their risks can usually explain the control strategy, the evidence behind it, and the unresolved limitations. Generic assurances—especially when they conflict with what was observed on the floor—deserve follow-up.
For teams responsible for quality and safety, the best automotive supplier assessment produces more than an audit score or an approved-vendor decision. It creates a focused picture of where confidence is justified, where verification is needed, and where a seemingly minor control gap could become a vehicle-level issue. In exterior, wheel, tire, lighting, and sensing systems, that clarity protects not only a program schedule, but also the performance and trust drivers experience every day.