
Industry Portal
Related News
- 00
0000-00
ASPICE for Smart Optical Systems: Evidence Needed for Automotive Development - 00
0000-00
How to Select NVH Control Materials for Automotive Panels and Powertrain Systems - 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects
How to Evaluate a Vehicle Exterior Systems Manufacturer for OEM Programs
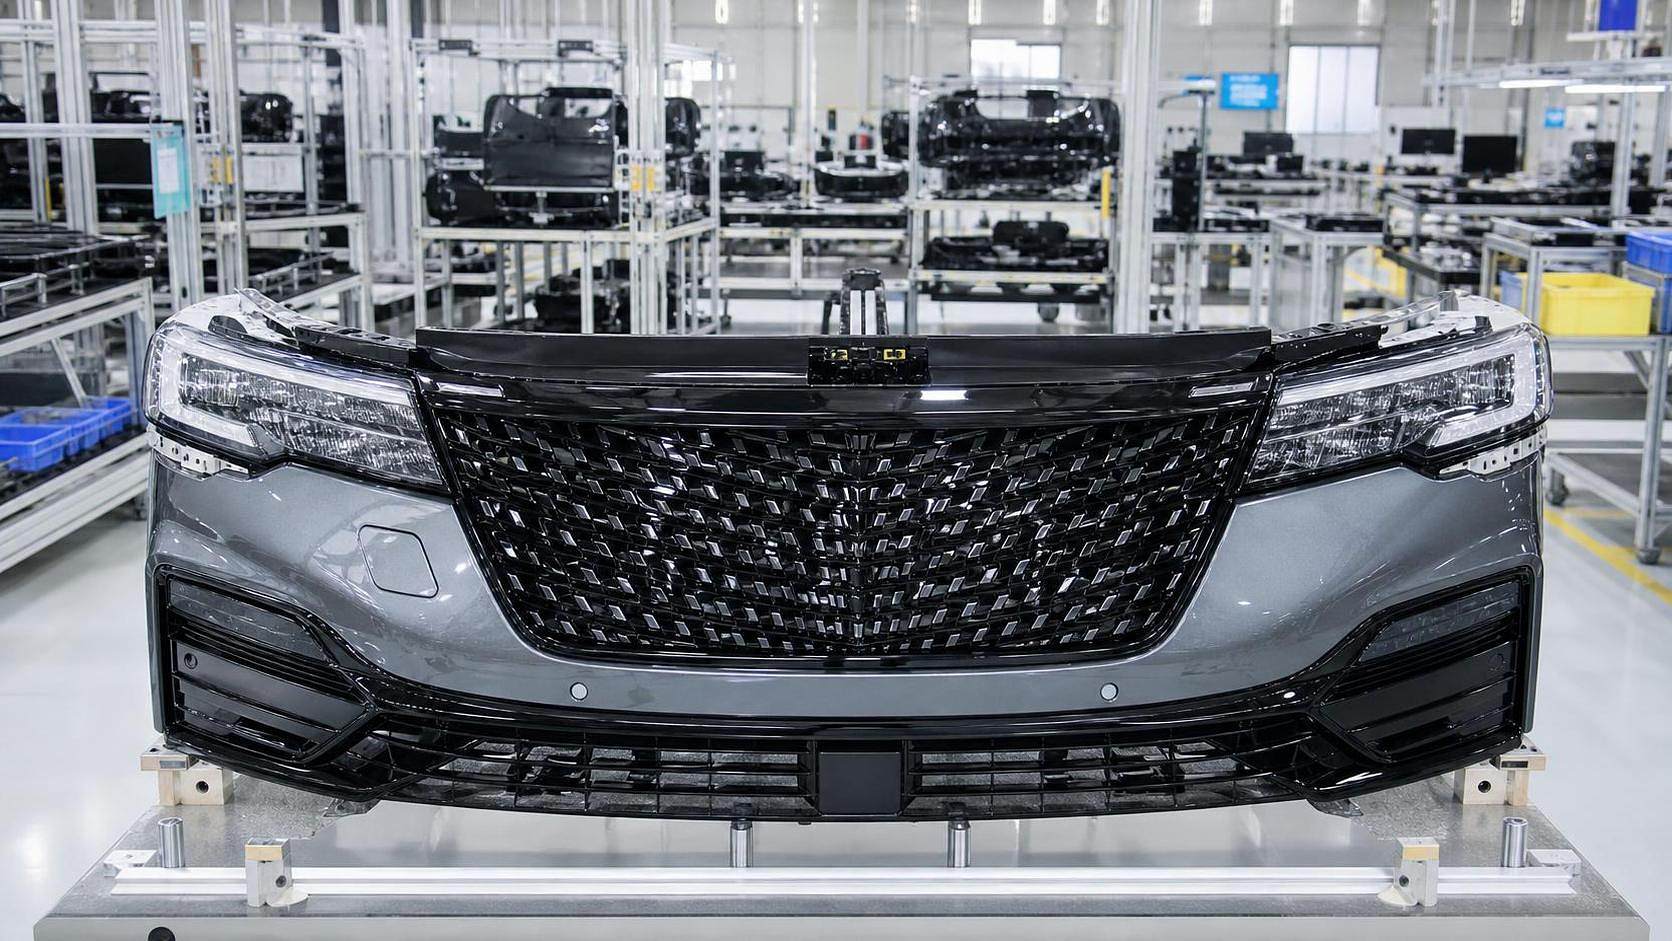
Cost pressure in an OEM program usually appears long before mass production. It begins when a vehicle exterior systems manufacturer quotes a part that looks competitive on paper but has weak control over tooling maturity, dimensional stability, optical performance, sealing, surface finish, or logistics discipline. Once those gaps surface in validation or launch, the apparent savings are often consumed by rework, line interruptions, engineering change requests, expedited freight, or field risk. A serious evaluation starts with total program exposure rather than unit price alone.
The first useful question is whether the supplier truly owns the technical depth of the product family being sourced. “Vehicle exterior systems” can cover very different categories: painted trim, grille assemblies, lamp housings, illuminated logos, sensor-integrated fascias, wheel-related aerodynamic covers, roof modules, mirror subassemblies, and sealing interfaces around movable exterior parts. A manufacturer that performs well in low-complexity molded trim may not be ready for components that combine optics, electronics, thermal paths, decorative Class A surfaces, and tight vehicle gap-and-flush requirements. The evaluation has to stay tied to the exact subsystem, not to a broad corporate capability statement.
Start with engineering ownership, not brochure capability
For OEM programs, engineering ownership matters because many exterior failures are designed in before they are ever produced. Ask how the supplier controls stack-up at attachment points, manages thermal expansion across mixed materials, and protects visible surfaces during assembly. For lamp-adjacent parts, review how heat, venting, and condensation paths are considered. For radar- or camera-facing covers, examine resin selection, wall thickness consistency, pigment effects, and the treatment of sink marks or knit lines that may affect signal transmission or appearance.
Tooling discussion should also go deeper than cavity count and lead time. A capable supplier can explain gate location logic, weld-line placement, cooling balance, warpage risk, venting, and how tooling design supports repeatable shut lines on the vehicle. If a decorative exterior part relies on paint, plating, texture, hard coat, or black gloss finishing, the team should be able to describe where cosmetic risk sits in the process and how it is contained. Vague answers here usually mean later disputes over whether a defect is a design issue, a process issue, or an unreasonable expectation.
Early design collaboration is another strong signal. A mature supplier will challenge impossible section transitions, excessive gloss sensitivity, hidden clip serviceability, or tolerances that stack up badly at the body side. That kind of pushback is useful. Silence during design review often becomes noise during launch.
Assess manufacturing around consistency, not nameplate capacity
Large stated capacity says little unless it is connected to the actual process route. Exterior systems often pass through multiple risk points: injection molding, die casting, stamping, painting, metallization, ultrasonic welding, adhesive bonding, leak testing, electronic calibration, functional inspection, packaging, and sequence control. The important issue is whether those steps are linked through stable work instructions, fixture discipline, traceability, and reaction plans when variation appears.
During a plant review, watch the production floor for evidence of process control rather than polished presentations. Look at part containment near paint lines, handling methods for piano-black or lens surfaces, mold maintenance records, fixture wear tracking, and quarantine flow for suspect stock. If assemblies include clips, seals, vents, or threaded inserts, confirm that insertion and torque methods are controlled and recorded where needed. Exterior parts fail in ordinary ways: clips crack after material drift, seals twist in assembly, gloss shifts between batches, chrome-like finishes haze after transport, and bonded joints weaken because surface preparation changed without a formal update.
Production consistency is especially important where lightweight exterior content intersects with EV architecture. Aluminum decorative or structural exterior elements may require close control of porosity, coating adhesion, corrosion resistance at mixed-metal joints, and dimensional movement after machining. Sensor-related covers and smart lighting surrounds introduce another layer, where cosmetic perfection cannot come at the expense of electromagnetic or optical function.
Validate quality using real failure modes
A useful supplier assessment is built around known failure modes for the target part, not around generic quality claims. Exterior assemblies live through UV exposure, road salt, gravel impact, thermal cycling, car-wash chemicals, pressure washing, vibration, and repeated assembly handling. The right conversation is whether the manufacturer has a disciplined method for linking design features and process parameters to those conditions.
Ask to review control plans and failure analysis examples from similar parts, with confidential details removed if necessary. The substance matters: how surface waviness is measured, how gloss or color drift is judged, how seal compression is validated over time, how lens haze or condensation complaints are diagnosed, how clip retention is verified after aging, how adhesive cure windows are locked, and how lot traceability works when a defect is found at vehicle assembly.
Be careful with pass/fail language that hides instability. A part can pass a lab test once and still be unreliable in serial production if the process window is narrow. Better evidence includes margin understanding, process capability on critical dimensions, fixture repeatability, and a credible containment method when a deviation is detected. For visible exterior content, subjective appearance approval should be backed by controlled lighting, boundary samples, and agreed inspection distance, otherwise quality arguments multiply as soon as launch pressure rises.
Regulatory and homologation readiness should be practical
Exterior systems regularly touch compliance areas involving lighting, visibility, impact behavior, pedestrian interfaces, wheel and tire fitment zones, labeling, and material restrictions. The supplier does not need to own every final approval activity, but it should understand how its component influences those outcomes. When evaluating a vehicle exterior systems manufacturer, look for structured document control around material declarations, design revisions, validation records, and production changes that could affect compliance-relevant characteristics.
This becomes more sensitive in programs spanning multiple markets. A component geometry, marking detail, reflective behavior, optical output interface, or sensor cover material that is acceptable in one region may require adjustment elsewhere. The practical question is whether the supplier can manage variant complexity without mixing parts, mislabeling packaging, or introducing undocumented substitutions. A weak configuration management system is a launch risk even when the underlying part design is sound.
Cost analysis should follow the process route
A quotation only becomes meaningful when broken into process logic. Review the likely cost drivers: resin grade, alloy type, coating chemistry, electronic content, cavity utilization, cycle time assumptions, scrap exposure on cosmetic surfaces, post-processing labor, test burden, and packaging design. Exterior programs often hide cost in non-obvious places. A glossy decorative finish may demand higher rejection allowances. A complex lamp bezel may need protective interlayers in packaging. A large painted fascia component can consume warehouse space and suffer transport scuffing if dunnage is poorly designed.
Tooling and launch cost deserve separate attention. Some suppliers suppress initial tooling numbers and recover them later through engineering changes, life-cycle claims, or expensive service parts. Others quote a low piece price based on assumptions that only work if annual volume, color mix, or logistics pattern stays ideal. It is worth challenging the assumptions behind scrap, maintenance, spare tools, gauging, service inventory, and end-of-line inspection. A lower quote with weak assumptions is not cheaper; it is simply less transparent.
Raw material volatility also matters in this category because aluminum, specialty polymers, coatings, rubber interfaces, optical-grade materials, and electronics can move on different timelines. The issue is not whether a supplier can predict the market, but whether the commercial structure clearly defines adjustment triggers, substitution approval rules, and inventory exposure when specification changes occur late.
Supply continuity depends on the lower tiers
Many exterior assemblies are only as stable as their second- and third-tier inputs. Resin compounds, coatings, LEDs, sensors, vents, clips, adhesives, fasteners, and decorative films may each come from different sources with different change-control habits. Ask for a realistic map of the upstream chain, especially for single-source or long-lead items. If a manufacturer claims strong vertical integration, verify which operations are truly internal and which are managed through satellite partners.
Business continuity planning should be concrete. That includes alternate tooling strategy where justified, preventive maintenance discipline, backup utilities for critical operations, emergency containment routines, and the ability to segregate conforming stock quickly. Exterior parts with sequenced vehicle variants add another risk: a supply issue may not stop all production immediately, but it can shut down specific trims or option packages in a way that creates disproportionate disruption.
Launch support reveals the real operating standard
The transition from approved samples to serial build is where many weak suppliers are exposed. Evaluate how the manufacturer supports PPAP-equivalent milestones, trial builds, dimensional buy-off, plant-resident issue response, and engineering change implementation. Exterior systems often show problems first at vehicle assembly, where fixture interaction, body variation, operator access, and final appearance all meet at once. A supplier that reacts slowly, sends only commercial contacts, or cannot isolate root cause by cavity, line, shift, or material lot will consume valuable launch time.
Service parts planning should also be part of the evaluation. Exterior components are vulnerable to transport damage, repair demand, and late-running design updates. If left unmanaged, that creates confusion between production parts and aftersales variants, especially when color, gloss, sensor cutouts, or trim details change. A disciplined manufacturer can explain how service stock is identified, packed, and revision-controlled without contaminating serial supply.
Commercial discipline matters as much as technical strength
A manufacturer may have solid engineering but still create program risk through poor commercial control. Review how it handles change requests, claim resolution, packaging liability, freight responsibility, and recovery logic for defects discovered after shipment. Exterior parts are particularly vulnerable to argument because damage can occur in molding, finishing, packing, transit, line-side handling, or vehicle assembly. Commercial terms should align with actual failure points, otherwise every issue becomes a negotiation instead of a correction.
Communication quality is a useful predictor. Clear revision histories, timely disclosure of process changes, and documented deviation approvals usually indicate a healthier operating culture than polished presentations. The best partner is often the one that exposes constraints early: a resin with long lead time, a finish with narrow yield, an adhesive with storage sensitivity, a wheel-surface treatment that complicates corrosion performance, or a sensor cover geometry that threatens optical clarity. That honesty protects the program.
When the evaluation is done properly, the strongest vehicle exterior systems manufacturer is rarely the one with the lowest starting number or the broadest marketing claim. It is the one that can connect design intent, process capability, appearance control, compliance discipline, supply continuity, and launch response into one coherent operating model. In OEM exterior programs, that coherence is what keeps cost from escaping later.