Industry Portal
Related News
- 00
0000-00
Fuyao Glass Granted Patent for Intelligent Sunroof Safety Response Device - 00
0000-00
Choosing a Precision Forging Supplier: Tolerances, Traceability, and Lead Times - 00
0000-00
NHTSA Proposes FMVSS 108 Update for Automated Vehicle Lighting - 00
0000-00
Replacement Headlight Assemblies for Sedans: Fitment Checks Before You Buy - 00
0000-00
Pirelli and BKT Reach Agreement to Enter India's Passenger Car Tyre Market
Choosing a Precision Forging Supplier: Tolerances, Traceability, and Lead Times
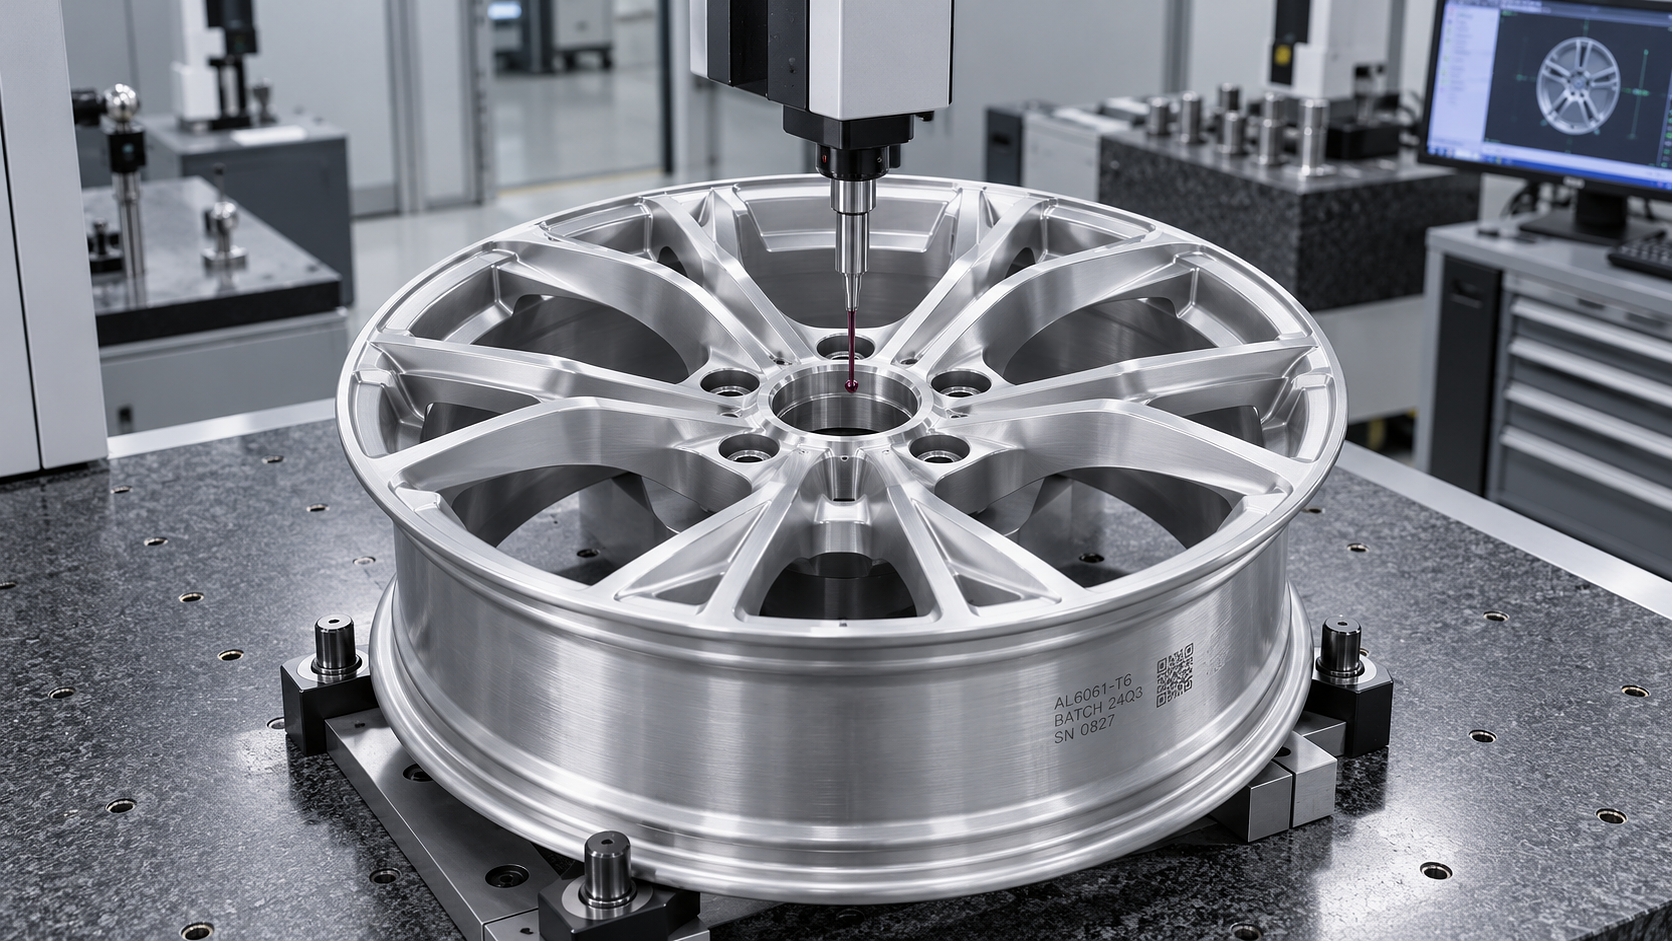
A precision forging supplier should be selected on demonstrated control of the finished component, not on the tightest tolerance advertised or the shortest lead time quoted. A competitive offer has limited value if critical dimensions depend on undocumented rework, material records cannot be connected to shipped parts, or the delivery promise excludes tooling approval and production validation.
The strongest comparison links three questions: which characteristics the supplier can control consistently, how the production history of each shipment can be reconstructed, and what must happen before conforming parts are ready for dispatch. For automotive lightweight components, including forged aluminum wheels, these questions must cover the complete manufacturing route—not just the forging press.
Define what the supplier is actually delivering
“Precision forging” does not describe a uniform supply scope. One quotation may cover a near-net-shape forging; another may include heat treatment, machining, surface finishing, inspection, and packaging. Comparing their unit prices without separating those responsibilities creates a false cost advantage.
Start with a controlled drawing revision, material specification, required delivery condition, estimated volumes, and the intended inspection and approval requirements. Identify whether dimensions apply to the as-forged blank, the heat-treated part, or the finished component. A tolerance that is achievable after machining says little about the dimensional capability of the forging operation itself.
For a forged aluminum wheel, for example, the manufacturing route may include billet preparation, forging, heat treatment, machining, finishing, and final inspection. Some designs also incorporate flow forming. The supplier should identify the proposed route explicitly rather than treating different processes as interchangeable under a broad “forged wheel” description.
Require a written feasibility review before commercial nomination. It should identify drawing exceptions, proposed machining allowances, tooling assumptions, outsourced operations, and characteristics requiring additional validation. A supplier that challenges an impractical requirement with a technically supported alternative provides more useful evidence than one that accepts every drawing note without qualification.
Assess tolerances at the feature level, not through a headline claim
A statement such as “high-precision capability” is not an acceptance criterion. Dimensional performance depends on alloy, geometry, part size, die configuration, thermal conditions, tool wear, and subsequent processing. A capability demonstrated on a small machined feature cannot be transferred automatically to a large, thin-section forging.
Separate the drawing into characteristics controlled primarily by forging, those established by machining, and those affected by later processing. Heat treatment can introduce distortion; machining can release residual stress; coatings can affect dimensions at mating surfaces. Inspection must therefore occur at the stage that represents the contractual requirement.
For wheels, mounting-face geometry, center-bore relationships, bolt-pattern position, and specified radial or lateral runout can affect fit and operation. These requirements need agreed datums and measurement setups. Two inspection reports can disagree even when both instruments are calibrated if the part is located or restrained differently.
Distinguish a successful sample from a capable process
A first-article report shows that the measured sample met the stated requirements. It does not establish that serial production will remain within them. Ask whether sample parts were produced using the intended equipment, tooling, material condition, heat-treatment route, and machining fixtures. Individually adjusted samples offer limited evidence of routine production performance.
Where statistical capability is required, agree on the relevant characteristics, sampling basis, acceptance thresholds, and treatment of non-normal data. Capability indices are meaningful only when the measurement system is suitable and the underlying process behavior is understood. A single favorable Cpk value, without the data distribution or production context, is weak evidence.
Measurement-system studies should address the actual inspection task. Depending on the feature, this may include gauge repeatability and reproducibility, fixture repeatability, instrument resolution, or correlation between supplier and receiving inspection. For critical features, align the measurement method before approval rather than after a rejected shipment.
Also ask how conformity is maintained as dies and cutting tools wear. Defined inspection intervals, replacement criteria, reaction plans, and segregation rules are stronger controls than a promise to inspect everything at the end. Final inspection can identify some nonconforming parts; it cannot make an unstable process reliable.
Make traceability prove a connection, not merely produce a certificate
A material certificate establishes reported properties for an identified material lot. It does not, by itself, prove that the delivered components came from that lot or received the specified processing. Effective traceability connects incoming material to production batches, heat-treatment loads, inspection results, and shipment identification.
Ask the supplier to demonstrate that connection using an existing, suitably redacted production record. Select a finished-part or shipment identifier and request the associated material documentation, manufacturing route, heat-treatment records, inspection status, and any authorized deviations. Then reverse the exercise: identify an incoming material lot and determine which finished shipments contain it.
The reverse search matters because it defines the potential containment scope when a material or process concern emerges. If records cannot distinguish affected from unaffected shipments, a narrowly originating issue can require a much broader quarantine.
Traceability granularity should match the component risk and contractual requirements. Batch-level identification may be sufficient for some applications; others require individual serialization. More detailed marking is not automatically better if identifiers become illegible after blasting, machining, coating, or service exposure. The identification method must survive the relevant manufacturing stages without creating an unacceptable surface defect or stress concentration.
Particular attention is needed when material batches are split, work-in-progress is combined, parts are reworked, or operations move outside the supplier’s facility. The records should preserve those relationships. Replacing a batch label after processing without maintaining its original linkage defeats the purpose of traceability.
Keep material identity separate from product performance
Correct alloy chemistry does not establish that the finished part has the required mechanical properties or structural performance. Heat-treatment condition, grain flow, local deformation, defects, and geometry can all matter. Specify which test results must accompany delivery and which belong in the qualification package, including any required specimen location and test frequency.
For automotive wheels, fatigue and impact validation must be addressed according to the applicable market, vehicle program, and customer requirements. A passing material test cannot substitute for required component-level validation. Equally, dimensional approval should not be interpreted as approval of structural performance.
Use certifications to verify scope, not replace qualification
ISO 9001 or IATF 16949 certification, where applicable, can support confidence in a supplier’s management system. Neither certificate proves that a particular forging meets its drawing, performance requirements, or destination-market obligations.
Check certificate validity, the named manufacturing location, the certified scope, and whether the operations being purchased fall within it. A certificate held by a related company or a different site does not automatically cover the proposed production route.
Where production part approval process documentation is required, agree on submission expectations and customer-specific requirements before scheduling approval. Clarify responsibility for process-flow documentation, risk analysis, control plans, measurement studies, material results, and performance testing. Missing approval evidence can block production release even when sample dimensions are acceptable.
Build lead time from dependencies rather than a single number
A credible lead time distinguishes new-program industrialization from repeat-order production. New tooling, trial forgings, corrective machining, testing, and approval create dependencies that do not exist in an established replenishment order. Combining them into one unexplained delivery estimate conceals the most important scheduling risks.
Require a milestone schedule showing when engineering inputs must be frozen, when tooling is released, when trial parts become available, and what evidence is needed for production authorization. Clarify whether the quotation includes an allowance for tool correction and repeat validation. A schedule that assumes every first trial succeeds provides little protection against launch disruption.
For repeat orders, examine the actual constraints: material availability, forging campaign schedules, heat-treatment capacity, machining availability, finishing queues, and inspection release. Press capacity alone does not establish finished-part capacity. A supplier may have available forging time but depend on an overloaded external heat-treatment or coating provider.
Ask for delivery performance measured against the original confirmed date, with definitions covering quantity completeness and quality acceptance. Performance measured only against revised dates can conceal schedule instability. Historical results are most useful when they relate to comparable products and the same manufacturing route.
- Order-release conditions: State whether timing begins after purchase-order acceptance, deposit receipt, drawing approval, or material authorization.
- Approval dependencies: Allocate review periods for samples, test results, and deviations rather than leaving them outside the schedule.
- Shipment readiness: Define whether completion means manufacturing finished, quality released, packed, or handed to the carrier.
- Transport assumptions: Identify the Incoterms rule, named place, transport mode, and responsibilities affecting the required arrival date.
Buffer inventory should follow the replenishment risk, not an arbitrary number of weeks. Finished stock may be valuable when machining or finishing is the bottleneck; reserved raw material may help when alloy availability is the constraint. Neither arrangement is dependable unless ownership, segregation, replenishment triggers, and treatment of engineering changes are agreed.
Make the commercial award reflect the evidence
Normalize quotations around the same delivery scope before evaluating price. Include tooling, qualification testing, inspection documentation, packaging, freight responsibilities, and any recurring testing charges. Then examine yield assumptions: a low forging price can lose its advantage if inconsistent stock allowance increases machining time or scrap.
Tooling terms also affect supply continuity. Define ownership, maintenance responsibility, expected replacement arrangements, storage, and access if production moves. Ownership alone does not guarantee practical transferability; drawings, process knowledge, compatible equipment, and validation may still be needed at another source.
Use unresolved technical issues as award gates rather than allowing a weighted commercial score to hide them. A supplier lacking traceability for a critical component should not compensate for that gap with a lower price. Conversely, a supplier with suitable controls but incomplete production validation may justify a conditional award, limited pilot quantity, and explicit release criteria.
Before serial supply begins, incorporate the agreed drawing revision, acceptance criteria, traceability requirements, approval obligations, change-notification rules, and delivery milestones into controlled purchasing documents. Require notification before changes to material source, production site, key processes, or subcontractors where those changes could affect conformity.
The defensible choice is the supplier whose demonstrated manufacturing route matches the part requirements and whose commitments remain clear when something goes wrong. Feature-level tolerance evidence, retrievable production records, and a dependency-based delivery plan provide a stronger basis for that decision than an attractive sample and an optimistic quotation.