Industry Portal
Related News
- 00
0000-00
Precision Forging for Aluminum Wheels: Alloy Selection and Fatigue Performance - 00
0000-00
NEV Industry Standards in China: Which Battery Safety Tests Are Required? - 00
0000-00
Automotive Exterior Lighting Systems: Lamp Types, Functions, and Placement - 00
0000-00
Choosing an Electric SUV Sunroof: Key Fit, Safety, and Weather-Sealing Factors - 00
0000-00
Pop-Up Automotive Sunroof Systems: Key Design Factors for Vehicle Integration
Supplier Capability Evaluation Matrix: Criteria and Weighting for Reliable Sourcing
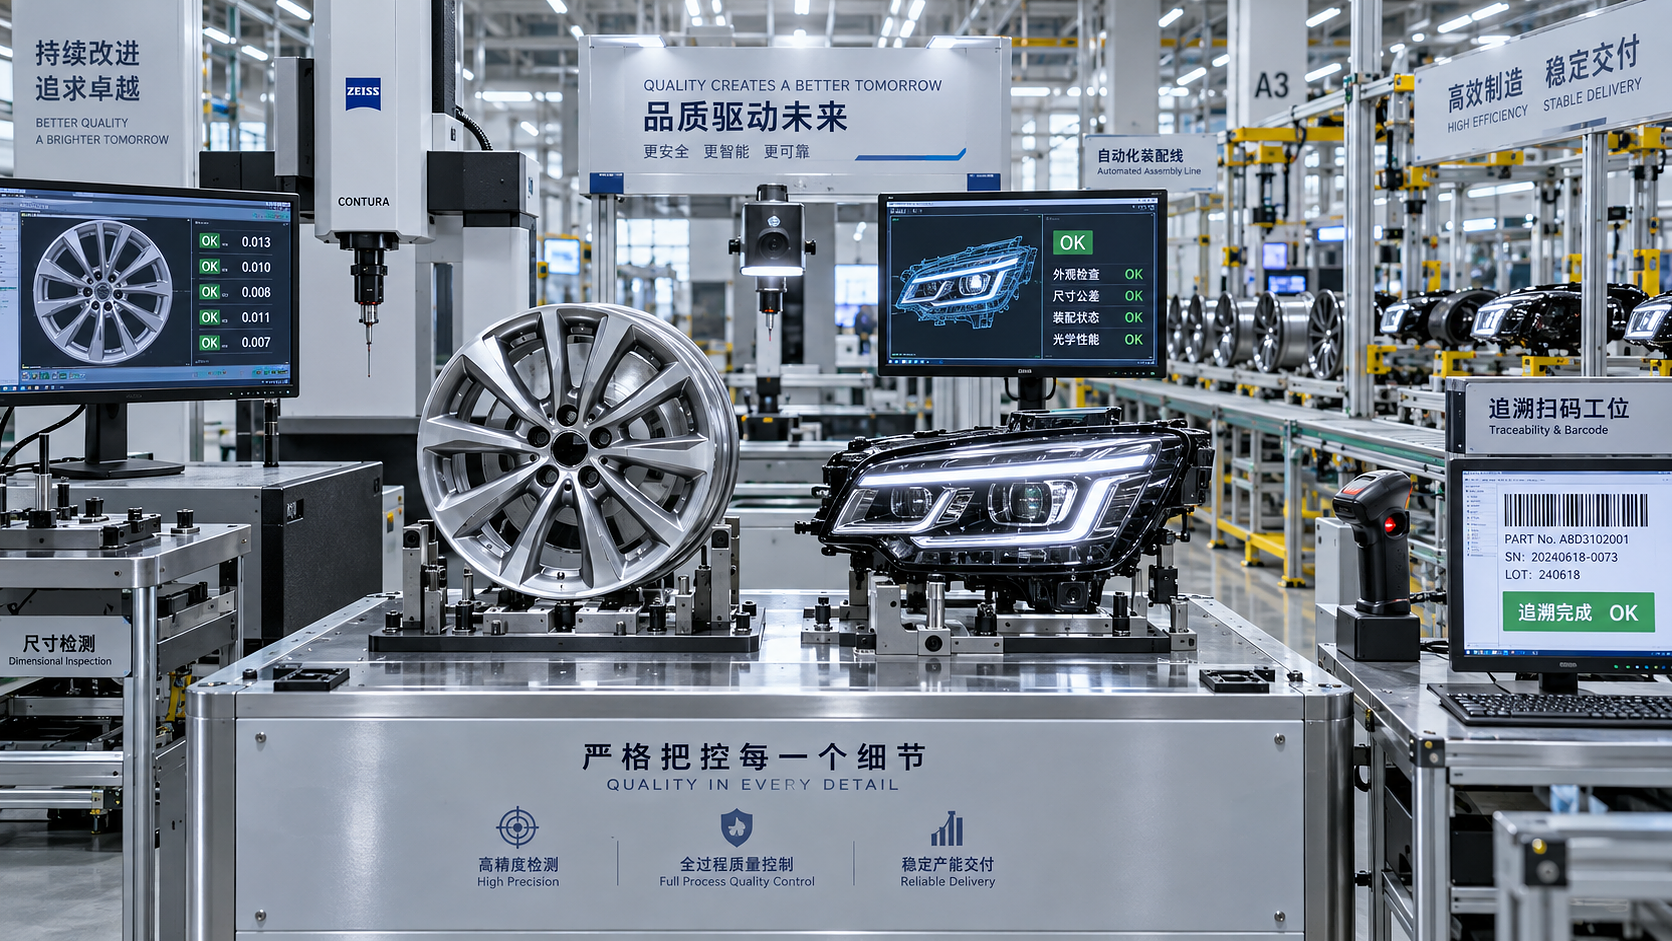
A sourcing decision can look settled when one supplier has the lowest quoted price, acceptable samples, and a familiar quality certificate. The risk often appears later: a wheel program encounters capacity pressure during launch, a headlamp supplier cannot demonstrate traceability for a design change, or a tire source meets laboratory targets but struggles to hold compound consistency across production batches. For exterior and vision components, these failures affect vehicle approval timing, warranty exposure, and plant continuity—not only piece price.
A supplier capability evaluation matrix prevents that narrow decision. It converts the requirements of a specific sourcing package into weighted, evidence-based criteria, then compares qualified suppliers on the factors most likely to determine reliable performance over the life of the program. Price should remain in the matrix, but it should not be allowed to outweigh technical fit, compliance control, delivery resilience, and change-management discipline.
Start with the sourcing risk, not a generic scorecard
The same matrix should not be used unchanged for forged wheels, panoramic roof assemblies, matrix LED lamps, EV tires, and sensor switches. Each category has a different failure path. A wheel supplier may be technically strong yet lack process control for cosmetic finishing and runout consistency. A smart lighting supplier may have robust electronics capability but limited capacity for optical validation, thermal testing, or regulatory documentation. A tire source may quote competitively while relying on a constrained rubber or reinforcement-material supply chain.
Before assigning weights, define what failure would be most damaging in the intended application. Procurement should work from the approved technical specification, production volume profile, launch schedule, target market, and required ECE, DOT, or other applicable regulatory obligations. This gives the evaluation team a reason to weight criteria differently rather than treating every line item as equally important.
For example, a replacement-parts purchase with a stable, fully validated design may place more weight on service level, inventory availability, and price stability. A new NEV headlamp assembly with adaptive or matrix functions should place greater weight on engineering depth, software and hardware change control, photometric validation capability, and compliance readiness. The supplier with the highest total score is only meaningful when the scoring logic reflects that distinction.
Build the evaluation gate before scoring suppliers
Some requirements should be treated as pass/fail gates rather than weighted advantages. A supplier that cannot meet a mandatory requirement should not remain competitive merely because it has a low-cost proposal or strong presentation. This is especially important where the component affects vehicle safety, road legality, structural integrity, or factory sequencing.
Typical gates include:
- Acceptance of the required drawings, specifications, and validation scope without unresolved technical exceptions.
- Evidence that the supplier can support applicable regulatory and market-entry requirements for the component and destination market.
- A functioning quality-management system appropriate to the customer’s supplier approval rules.
- Legal, financial, and ethical due-diligence clearance under the buyer’s internal policy.
- Agreement to traceability, change notification, confidentiality, warranty, and audit requirements.
- Available manufacturing capacity within the required program timing, or a credible and reviewable expansion plan.
A gate does not need to imply that a supplier is poor. It may simply mean the supplier is unsuitable for that package at that point in time. Keeping gates separate also prevents evaluation meetings from becoming negotiations over whether a critical gap can be offset by points elsewhere.
A practical weighting model for automotive exterior and vision sourcing
Once suppliers pass the gates, use a score scale that evaluators can apply consistently. A five-point scale is often sufficient: 1 indicates major weakness or unsupported claims; 3 indicates acceptable evidence with manageable limitations; 5 indicates demonstrated strength directly relevant to the package. Define the evidence required for each rating before reviewing submissions. Otherwise, one evaluator may give a 5 for a polished capability deck while another reserves a 5 for audited production proof.
The ranges are not a universal formula. They are a starting point for a controlled discussion. For a commodity-like, mature part, commercial stability may reasonably receive more weight. For a component with a demanding optical function or new material architecture, technical and quality criteria should dominate. The sum of all weights must equal 100%, and any change to weighting after suppliers are known should be documented and justified to avoid a biased outcome.
Score technical capability with evidence tied to the actual part
Technical capability should answer a narrower question than “Can this supplier make similar products?” The useful question is whether it can reliably make this product within its intended tolerances, duty cycle, appearance standard, and validation conditions.
For aluminum alloy wheels, examine the proposed manufacturing route, alloy control, tooling approach, machining capability, coating process, dimensional inspection, fatigue and impact validation arrangements, and experience managing cosmetic surfaces. Where low-drag wheel geometry is important, assess whether the supplier can maintain complex styling and aerodynamic features without compromising structural performance or production repeatability.
For electric sunroof systems, technical review should cover mechanical architecture, sealing, drainage, glass handling, motor and control integration, wind-noise management, durability testing, and serviceability. A supplier may offer a visually similar roof system but have limited evidence for the required opening cycles, water management, or NVH expectations.
For LED headlamp assemblies, capability includes optical design and measurement, thermal management, electronic reliability, condensation control, aiming mechanisms, software configuration where applicable, and the ability to validate beam performance across manufacturing variation. A proposal should make clear which tasks are performed internally and which rely on external laboratories or sub-suppliers. External support is not automatically a weakness, but it introduces interface and timing risk that the matrix should reflect.
For tires and sensor switches, do not accept broad statements about EV readiness or smart functionality. Ask for package-specific evidence: load and speed requirements, rolling-resistance and noise targets where specified, compound and carcass control for tires; sensing range, environmental robustness, electromagnetic compatibility interfaces, and diagnostic behavior for switches. The objective is not to request unnecessary confidential detail; it is to establish whether the supplier understands the engineering problem well enough to control it.
Quality capability is more than certification status
A certificate may support supplier eligibility, but it does not show how a factory reacts when a critical dimension drifts, a coating defect rises, or an incoming material lot changes. The matrix should distinguish documented systems from operating discipline.
Useful evaluation evidence includes process-flow diagrams, control plans, inspection methods, gauge management, traceability examples, nonconformance handling, corrective-action records, and the link between production data and shipment release. During a site assessment, pay attention to whether operators, quality personnel, and production supervisors describe the same controls. Inconsistent explanations can reveal that the documented process is not fully embedded.
Traceability deserves added weight for components where a field concern may require rapid containment. The buyer should know whether the supplier can trace a finished unit to its key materials, production date or shift, relevant equipment, inspection outcome, and major subcomponents. For a complex lamp or sensor assembly, serial-level traceability may be necessary. For other products, batch-level traceability may be sufficient, but the required level should be specified rather than assumed.
Test delivery resilience beyond stated annual capacity
A supplier can have enough theoretical annual capacity and still fail a launch. The useful review considers the production ramp, peak weekly demand, changeover loss, scrap allowance, maintenance downtime, labor availability, packaging flow, and transport lead time. It also identifies which operation is the real constraint. In a wheel plant, it may be finishing or inspection rather than casting. In a lamp assembly, it may be a particular optical module, electronic driver, or end-of-line test station.
Ask suppliers to map the critical path from purchased material to dispatched product. Then examine dependencies that are outside their direct control: single-source LEDs, lenses, rubber compounds, electronic components, coatings, forging billets, or specialized tooling. A supplier does not need to own every process, but it should show how it monitors critical sub-suppliers, qualifies alternates where permitted, and communicates disruptions.
Delivery resilience also includes logistics behavior. Check whether packaging protects optical surfaces, painted components, seals, and finished wheel faces; whether shipment frequency matches plant consumption; and whether the supplier can separate urgent containment stock from normal production inventory. These practical details often matter more than a general statement about supply-chain flexibility.
Keep commercial scoring transparent without rewarding hidden risk
The commercial section should compare total cost rather than unit price alone. Include tooling, development charges, packaging, freight assumptions, customs exposure where applicable, payment terms, warranty allocation, service-part obligations, and the cost of required validation or changes. A quote that excludes foreseeable engineering support may look attractive in the matrix while shifting cost and schedule risk to the buyer later.
Raw-material exposure needs its own review for aluminum wheels, rubber-intensive products, glass, optical polymers, and electronic content. Procurement should understand whether price adjustments are fixed, indexed, capped, or open to unilateral revision. The purpose is not to force every supplier into the same mechanism; it is to compare the predictability and auditability of each proposal. A low initial quote with vague adjustment language deserves a lower commercial stability score than a slightly higher quote with clear assumptions.
Use a two-stage review to avoid false precision
Weighted totals are valuable, but they can create an illusion of certainty. A supplier scoring 82 versus 79 is not automatically the better choice if the difference comes from subjective ratings or if the lower-scoring option has a stronger position on a non-negotiable operational risk. A two-stage review handles this better.
- Individual scoring: Engineering, quality, supply chain, purchasing, and program representatives score independently against the agreed definitions. They should record evidence and open questions beside each score.
- Calibration discussion: The group compares major scoring gaps, reviews the evidence, confirms the weighted result, and identifies risks that require mitigation before nomination.
The output should include more than a ranked list. Record the selected supplier, the reasons for selection, conditions of award, unresolved actions, owners, due dates, and fallback options. An example condition might be completion of a process-capability review before tooling release, confirmation of second-source coverage for a key electronic part, or closure of a regulatory documentation gap before shipment approval.
When a lower-ranked supplier may still deserve a place
Dual sourcing, development sourcing, or a controlled trial can be justified when the matrix identifies a strategic capability that the leading supplier does not offer. A supplier with lower current capacity may have superior optical engineering; another may offer a more stable regional logistics route; a third may be better suited to aftermarket packaging and service-part responsiveness. The decision should state the intended role clearly instead of treating all approved suppliers as interchangeable.
The matrix should also be updated when the program changes. New markets, a revised styling surface, tighter energy-efficiency targets, a software feature, or a revised volume forecast can alter the risk profile. Reusing the original scorecard without revisiting its weights may preserve a decision logic that no longer matches the part being sourced.
A reliable evaluation process is not the one with the most criteria. It is the one where each weight reflects a real sourcing consequence, each score can be supported by evidence, and critical weaknesses are converted into explicit approval conditions rather than buried inside an average.