
Industry Portal
Related News
- 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions
Photoelectric Sensing Failures in Dusty Lines: Causes, Fixes, and Prevention
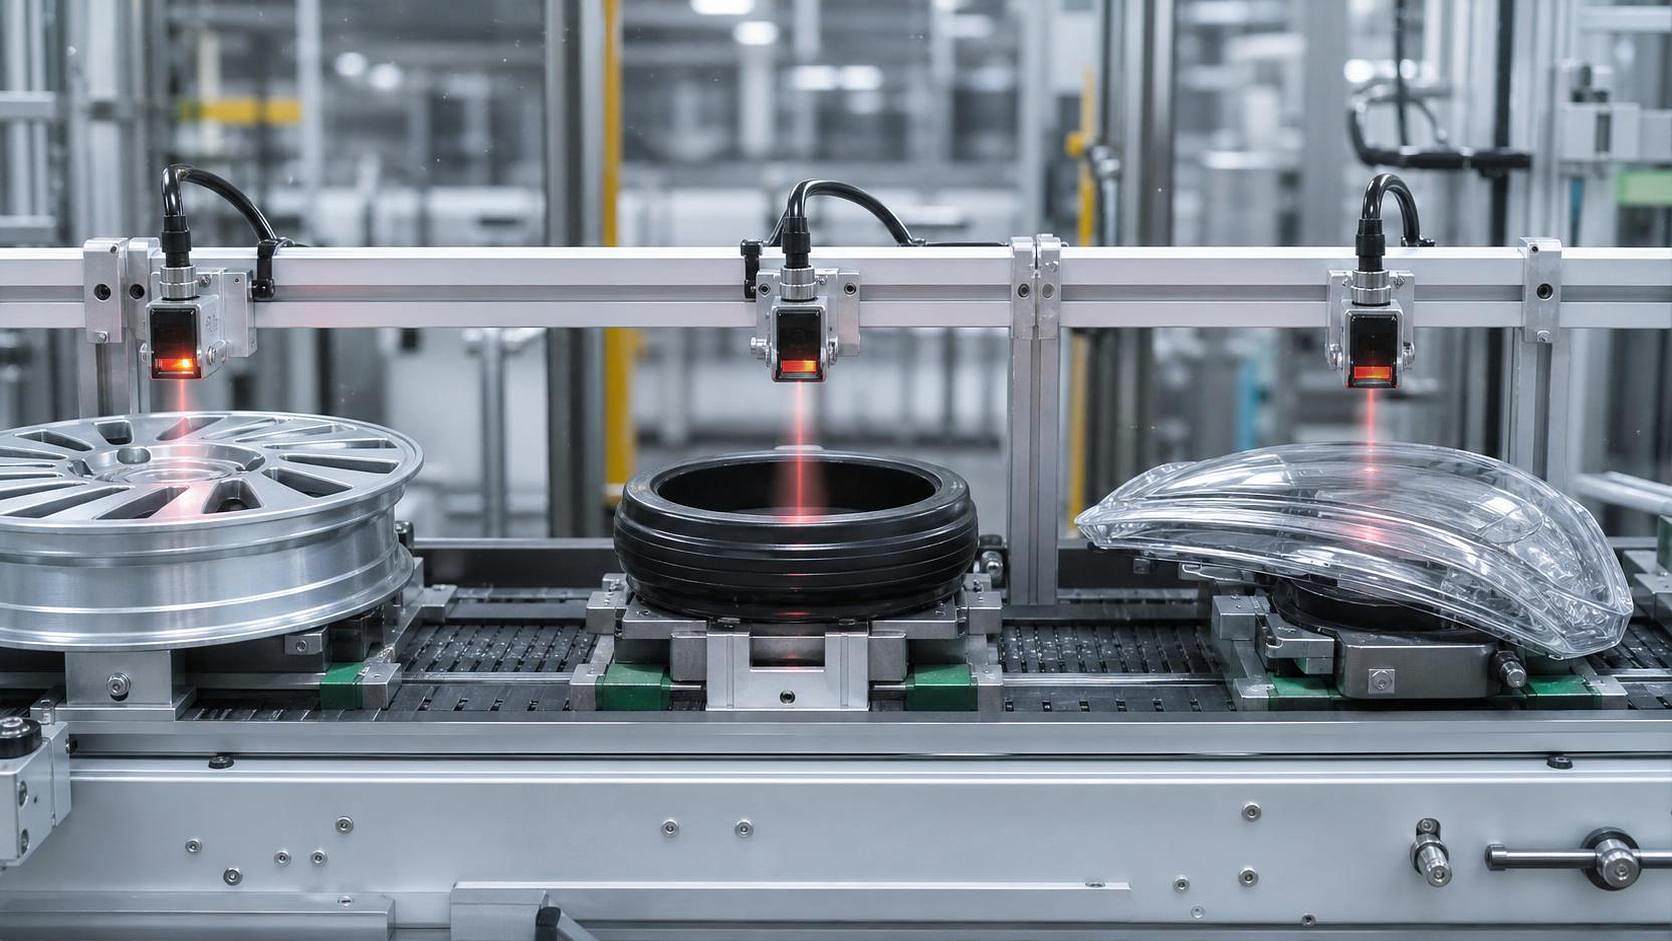
Why photoelectric sensing fails faster on dusty lines
On dusty lines, photoelectric sensing rarely degrades all at once. It usually drifts first, then starts creating false triggers, missed parts, and unstable cycle timing.
That pattern matters in automotive-related production, where optical reliability supports both output stability and traceable quality control.
Within the broader AEVS view of smart optical perception, sensor performance is not an isolated maintenance issue. It affects process confidence across exterior components, lighting modules, and sensor switch assembly.
A dusty wheel finishing cell does not stress photoelectric sensing the same way as a headlamp inspection station or a packaging conveyor for sensor subassemblies.
The practical question is not whether dust is present. The real question is how dust interacts with target shape, surface reflectivity, mounting angle, vibration, and cleaning intervals.
Different line conditions create different photoelectric sensing risks
In actual operations, dust behaves differently depending on the process. Fine metallic powder, rubber residue, polishing mist, and cardboard fibers do not interfere with optics in the same way.
That is why one photoelectric sensing setup performs well in one area and becomes unreliable a few meters away.
Wheel machining and finishing lines
Aluminum wheel production often combines metallic dust, coolant mist, and vibration. Here, photoelectric sensing failures commonly start with lens contamination and weak signal margin.
Reflective surfaces add another complication. A polished rim can return unstable light, especially when sensor alignment shifts after repeated machine movement.
Tire handling and packaging zones
Tire areas produce rubber dust and dark, low-reflectivity targets. In these conditions, photoelectric sensing often struggles with contrast rather than simple obstruction.
A sensor that detects glossy trays accurately may miss black tread edges, sidewall markings, or irregular stacked shapes.
Headlamp and optical module assembly
LED headlight lines usually look cleaner, yet photoelectric sensing can still fail because transparent covers, glossy housings, and ambient light create optical ambiguity.
In these stations, the issue is often not heavy dust buildup. It is mixed interference from airborne particles, reflective surfaces, and tight detection tolerances.
Auto sensor switch assembly and testing
For auto sensor switches, small-part verification needs precise and repeatable photoelectric sensing. Dust here may be light, but tolerances are narrow and false acceptance is costly.
When housings, connectors, and clips vary in color or finish, the sensing window must be tuned for the part family, not for one sample.
The common causes are simple, but the root cause is usually not
Most photoelectric sensing failures in dusty environments come from a short list of conditions. The mistake is treating every alarm as a dirty lens problem.
- Dust accumulation on emitter or receiver windows reduces usable light and narrows operating margin.
- Target surfaces change over time, especially with oil film, metallic residue, or packaging abrasion.
- Mounting brackets loosen under vibration, causing gradual misalignment rather than sudden failure.
- Background reflections become stronger after layout changes, repainting, or replacing nearby guards.
- Compressed air cleaning is applied inconsistently, moving dust without truly removing it.
- Sensor selection ignores sensing mode, using diffuse sensing where through-beam or retro-reflective would be more stable.
More often, photoelectric sensing fails because several small factors overlap. A slightly dirty lens, a darker batch surface, and a shifted bracket can be enough.
What to check first when false triggers and missed detections appear
A useful field check starts with signal behavior, not assumptions. Watch whether the failure is constant, intermittent, or linked to one product variant.
If photoelectric sensing fails only during peak dust generation, contamination control is likely primary. If it fails after changeover, alignment or teach settings may be the real issue.
This kind of diagnosis is especially relevant for lines tied to exterior quality, where small detection errors can distort downstream traceability.
The best fix depends on how the line actually uses photoelectric sensing
There is no universal correction. Stable photoelectric sensing comes from matching the sensor method to the contamination profile and the target behavior.
When dust is heavy and constant
Use higher excess gain, stronger contamination tolerance, and protective mounting. Through-beam designs often outperform diffuse setups in these zones.
Air purge accessories can help, but only when airflow direction is controlled. Otherwise, dust simply circulates around the lens face.
When parts are glossy, curved, or transparent
Photoelectric sensing should be evaluated for reflection angle and background rejection. Polarized retro-reflective or specialized transparent-object sensing may be more reliable.
This is common in lamp covers, coated trims, and sunroof-related subassemblies, where optical behavior changes with surface treatment.
When changeovers are frequent
Settings must tolerate part variation without becoming too loose. One stable approach is to validate the darkest, brightest, and most offset samples before locking thresholds.
If that is not done, photoelectric sensing may look stable during setup and fail only after the next batch mix arrives.
Different scenarios call for different maintenance rules
Cleaning frequency should follow contamination rate, not calendar habit. A fixed weekly routine may be excessive in one area and dangerously late in another.
A simple comparison helps define realistic maintenance standards for photoelectric sensing across mixed production environments.
Where teams often misread the problem
One common mistake is choosing sensors by catalog range only. In dusty lines, nominal distance means little without contamination margin.
Another frequent error is assuming similar stations need identical photoelectric sensing. A tire transfer point and a headlamp verification nest may share footprint, but not optical demands.
Short-term fixes also create blind spots. Repeated cleaning may reduce alarms, while bracket movement or target variation remains unresolved.
Cost is often misread as well. Lower initial sensor price can lead to more stoppages, more resets, and more frequent replacement in harsh environments.
A practical way to prevent repeat photoelectric sensing failures
Prevention starts by mapping each detection point to its real exposure conditions. Dust type, target finish, motion path, and nearby reflections should be documented together.
- Rank sensing points by failure impact, not by sensor count.
- Record baseline signal condition after proper cleaning and alignment.
- Set inspection intervals based on contamination buildup speed.
- Retest after tooling changes, guard replacement, or product finish changes.
- Standardize mounting, cable routing, and cleaning method across similar stations.
For operations linked to automotive exterior and smart optical perception, this discipline matters because sensing quality supports larger system quality.
A reliable photoelectric sensing strategy helps maintain consistent assembly flow, cleaner inspection data, and fewer avoidable stoppages.
What to review before the next adjustment cycle
Before changing hardware, review where photoelectric sensing actually breaks down: contamination, contrast, reflection, alignment, or variation over time.
Then compare stations by real application conditions rather than by equipment label. That usually reveals why one dusty line stays stable and another does not.
The next useful step is to define a simple adaptation standard for each sensing point, including acceptable signal margin, cleaning interval, and revalidation trigger.
That approach turns photoelectric sensing from a recurring fault source into a controlled part of production reliability.