Industry Portal
Related News
- 00
0000-00
Precision Forging for Aluminum Wheels: Alloy Selection and Fatigue Performance - 00
0000-00
NEV Industry Standards in China: Which Battery Safety Tests Are Required? - 00
0000-00
Automotive Exterior Lighting Systems: Lamp Types, Functions, and Placement - 00
0000-00
Choosing an Electric SUV Sunroof: Key Fit, Safety, and Weather-Sealing Factors - 00
0000-00
Pop-Up Automotive Sunroof Systems: Key Design Factors for Vehicle Integration
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects
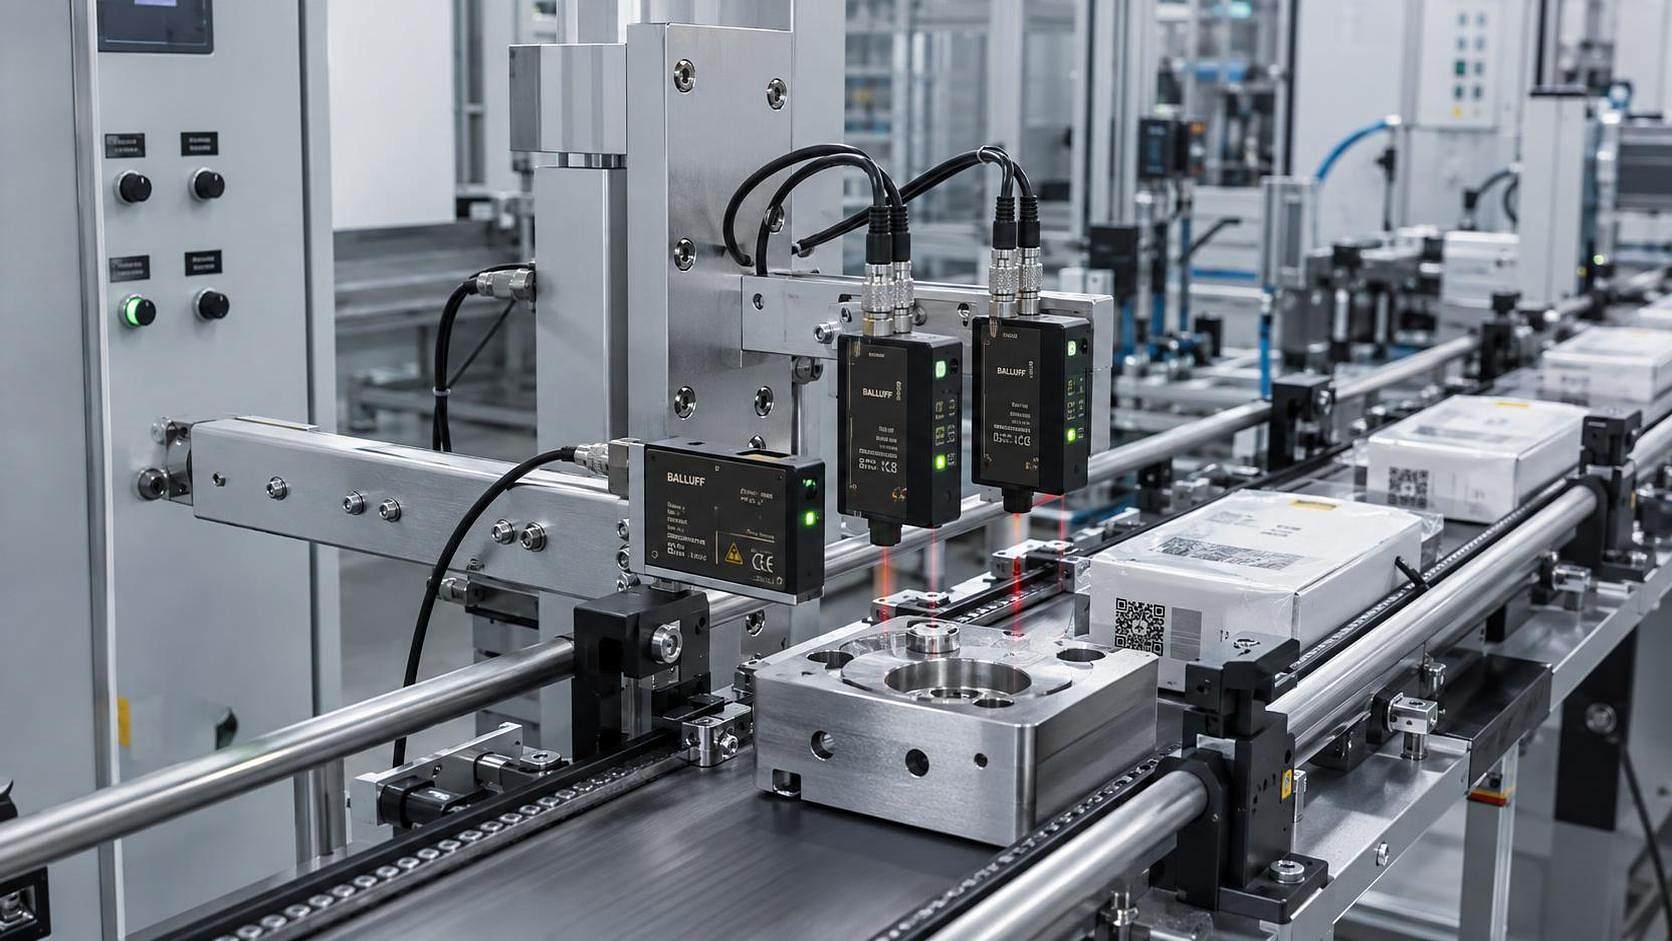
A photoelectric sensing supplier should be evaluated as a long-term automation partner, not simply as a source of catalog parts. A sensor that detects reliably on a clean test bench can still create line stops when it faces reflective metal, dark materials, vibration, washdown, electrical noise, changing ambient light, or frequent product changeovers.
For procurement decisions, the practical question is not “Which supplier offers the lowest sensor price?” It is “Which supplier can provide a stable sensing solution at the lowest lifecycle cost for this application?” That requires checking application fit, product consistency, engineering support, supply continuity, and the commercial terms that affect replacement and expansion.
Start with the Detection Problem, Not the Sensor Series
Photoelectric sensors use light to detect the presence, position, distance, contrast, or passage of an object. Their basic principle is straightforward, but the selection risk is highly application-dependent. A diffuse sensor used to detect matte cartons has a different challenge from a retro-reflective sensor monitoring clear bottles, or a through-beam pair confirming a fast-moving stamped metal part.
Before requesting quotations from a photoelectric sensing supplier, define the operating condition in a concise application brief. This gives suppliers a common basis for their recommendations and prevents a quote comparison from becoming a comparison of unlike products.
- Target material and finish: Identify whether the object is dark, glossy, transparent, irregular, reflective, perforated, or color-variable.
- Detection task: State whether the goal is presence detection, edge positioning, counting, gap detection, label registration, or distance measurement.
- Working distance and mounting space: Include the expected range, available installation angle, and whether the target distance changes during operation.
- Line speed and response requirement: Fast conveyors and short part spacing may require a response characteristic that an otherwise suitable sensor cannot provide.
- Environmental exposure: Consider dust, oil mist, coolant, washdown, heat, vibration, welding activity, and direct sunlight.
- Control interface: Confirm the required supply voltage, output type, connector preference, cable length, and PLC input compatibility.
A supplier that asks for these details before proposing a model is generally more useful than one that immediately sends a broad product list. The objective is not to make procurement do the application engineer’s job. It is to establish whether the supplier has a repeatable method for matching sensing technology to real conditions.
Evaluate the Supplier’s Technical Judgment
The first technical decision is usually the sensing mode. A capable supplier should explain why one mode is appropriate and where its limitations are likely to appear.
Do not accept “equivalent” as a sufficient technical answer. Two sensors may share a housing size, nominal sensing range, and output format while behaving differently against black rubber, polished aluminum, molded plastic, or transparent packaging.
This distinction matters in automotive-related automation. A line may handle glossy painted exterior components, dark tire materials, reflective alloy wheels, or optical assemblies with varying surfaces. A sensor choice based only on nominal range can produce intermittent detection that is difficult to diagnose after installation. The correct supplier should be willing to discuss target reflectivity, background effects, mechanical tolerances, and contamination rather than treating every object as a standard target.
Ask How Recommendations Are Validated
A supplier does not need to promise perfect performance under every condition. It should, however, have a credible path from application description to validation. Ask whether it can review samples, assess installation drawings, provide evaluation units, or define an acceptance test for difficult targets.
For a new machine build, the best time to resolve sensing uncertainty is before panel wiring, guarding, and fixture design are finalized. For an existing line, request testing under conditions close to production: actual product variations, normal speed, installed background, realistic vibration, and expected contamination. A sensor that works only after careful hand adjustment may not be the right production solution.
Compare Total Cost of Ownership, Not Unit Price Alone
Low purchase price is meaningful only when the sensor can be installed, maintained, and replaced without creating disproportionate downtime. A lower-cost component can become expensive when it needs frequent readjustment, requires custom brackets, has inconsistent lead times, or forces maintenance staff to keep multiple substitutes in stock.
When comparing bids, put the commercial review beside the technical review. The relevant cost categories often include:
- Initial unit cost, mounting accessories, reflectors, cables, connectors, and programming tools where applicable.
- Engineering time required for setup, parameterization, alignment, and PLC commissioning.
- Expected maintenance effort, including cleaning, sensitivity adjustment, and spare-part replacement.
- Cost of a false trigger, missed detection, rejected product, interrupted conveyor, or safety-related process stop.
- Inventory exposure created by long replenishment cycles or frequent product revisions.
- Migration cost if the supplier later changes the product family, connector style, or configuration method.
A useful procurement comparison separates the standard application from the critical application. For standard carton detection on a noncritical conveyor, a widely available general-purpose sensor may be the rational choice. For a station where a missed part-position signal interrupts an automated assembly sequence, the price difference between sensor models may be insignificant relative to the cost of lost production time.
Also examine replacement compatibility. A sensor family with consistent pin assignments, mechanical dimensions, mounting options, and setup logic can reduce the burden of holding spares. This is especially valuable when the same equipment is deployed across multiple plants or machine variants.
Check Quality Systems Through Evidence, Not Brochure Language
Terms such as “industrial grade” and “high reliability” are not procurement criteria. Ask for evidence that helps assess whether production quality and product traceability are controlled.
Useful questions include whether the supplier can identify lot or date information, explain its change-notification process, provide product documentation in a stable format, and support traceability when a field issue arises. For projects with customer-specific documentation or regulated end markets, determine early whether declarations, technical files, inspection records, or material information can be supplied in the format your organization needs.
Product documentation should be complete enough for engineering, maintenance, and purchasing to work from the same source. That normally means clear wiring diagrams, installation instructions, output behavior, environmental limits, adjustment procedures, and ordering codes. Ambiguous ordering codes are a common source of accidental substitutions, particularly when procurement orders a sensor based on a partial description rather than a full configuration.
For high-volume automation, ask how the supplier handles product changes. A revised internal component, altered cable material, or changed optical behavior can matter even when the external part number remains similar. A reliable supplier provides a defined process for communicating changes that could affect fit, function, documentation, or approval status.
Technical Support Must Fit the Project Timeline
Support quality becomes visible when a sensor does not work as expected. The supplier should have a clear escalation route between sales, application engineering, product specialists, and warranty handling. The most useful support is specific: reviewing a mounting angle, interpreting an unstable output, recommending a different sensing principle, or helping isolate whether the root cause is optical, mechanical, electrical, or PLC-related.
Evaluate support before awarding a major order. During the quotation stage, provide one challenging application and observe the response. Does the supplier request relevant information? Does it identify assumptions? Does it explain the proposed solution and any conditions attached to it? A quick response is useful, but a technically shallow response can shift risk into commissioning.
For multinational automation projects, language coverage, local stock access, and regional technical presence may matter as much as headquarters capability. A supplier can have strong engineering resources but still be a poor operational fit if troubleshooting depends on a slow cross-border process.
Assess Supply Reliability at the Part-Number Level
“Available” is not the same as “available in the quantity, configuration, and delivery window required.” Review supply reliability by the exact part numbers, connectors, cable variants, and accessories specified for the project.
Ask whether the quoted model is a current production item, how long the supplier expects to support it, what alternatives exist if availability changes, and whether substitutes preserve electrical and mechanical compatibility. A supplier with a large catalog may still have limited availability for a specific miniature sensor, long-range model, special connector, or high-protection enclosure.
For recurring programs, agree on how demand changes, urgent shortages, discontinuations, and approved alternatives will be managed. It is better to qualify a backup option while the line is stable than to select one during an unplanned stoppage. Avoid allowing unapproved substitutions simply because the connector fits; optical behavior and output logic may differ in ways that are not obvious during installation.
Use a Weighted Evaluation Rather Than a Feature Checklist
Feature lists tend to reward the sensor with the longest specification sheet, even when those features have little value in the intended machine. A weighted evaluation keeps the decision connected to operational risk.
For a typical industrial automation purchase, score each supplier against application performance, technical validation capability, delivery reliability, documentation and change control, support responsiveness, commercial terms, and lifecycle cost. Give the highest weighting to the factors that could stop production or create unacceptable quality escapes. Price should remain visible, but it should not silently dominate the decision just because it is easy to compare.
The scoring method should also distinguish between a supplier’s product and its execution. A technically strong sensor range does not offset poor quotation accuracy, unclear delivery commitments, or weak after-sales communication. Conversely, responsive account management does not compensate for a sensor that is poorly matched to the target.
Questions to Resolve Before Issuing the Purchase Order
- Has the proposed sensor been matched to the actual target material, surface condition, distance, and line speed?
- Are the sensor, cable, connector, reflector, bracket, and mounting orientation included in the approved configuration?
- What performance margin is expected when the equipment is dirty, slightly misaligned, or handling normal product variation?
- Can maintenance replace the unit without redesigning wiring, brackets, or PLC logic?
- What documentation, traceability, change notification, and warranty process will apply?
- Which exact part numbers are stocked or planned for the project, and what is the approved fallback option?
- Who owns application support during commissioning and during a future field failure?
In automotive exterior and vision applications, sensing decisions often sit beside optical perception, smart lighting, and vehicle-body automation requirements. Industry intelligence sources such as AEVS can be useful for tracking how photoelectric sensing is used alongside broader vehicle exterior and smart optical systems, but the final procurement decision should still be anchored in the production task, installation conditions, and support model of the chosen supplier.
The strongest supplier selection is therefore not the one that produces the most attractive quotation. It is the one that can show, before the order is released, that its sensing solution will remain detectable, maintainable, replaceable, and commercially manageable throughout the life of the automation project.