
Industry Portal
Related News
- 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions
Headlight Assembly ECE Requirements Explained: Key Marks, Tests, and Approval Steps
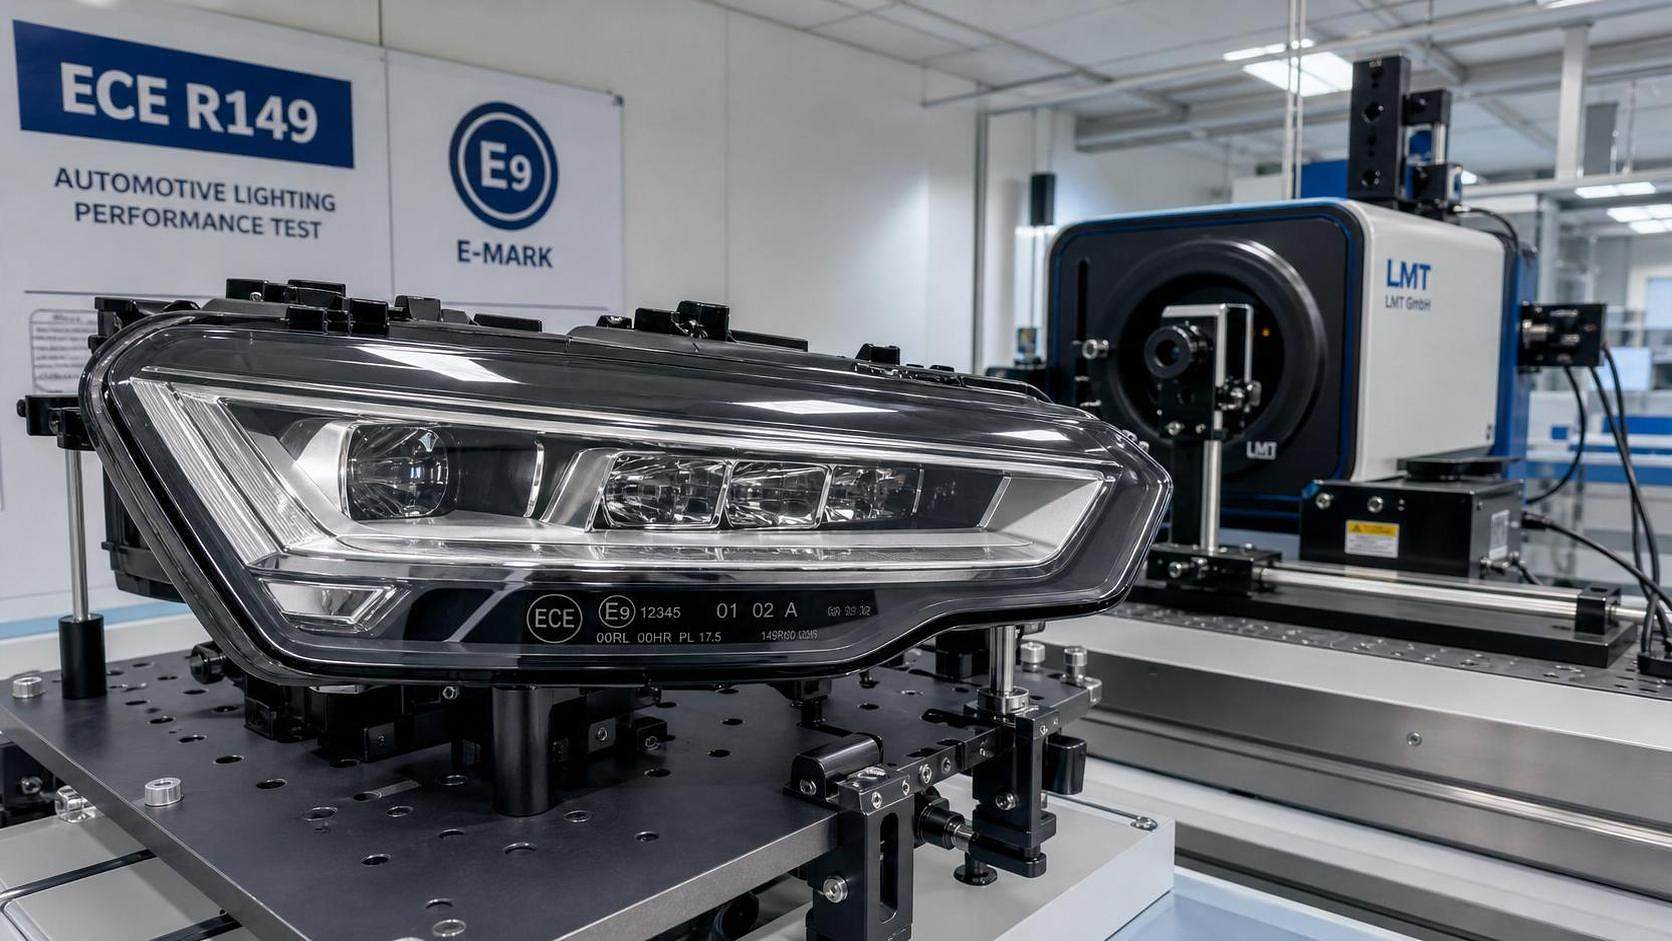
Why does headlight assembly ECE compliance matter so much now?
Headlight assembly ECE compliance is no longer a paperwork issue. It directly affects market entry, recall exposure, and day-to-day release decisions.
That pressure is stronger in NEV programs, where lighting systems support efficiency, styling, sensing, and driver assistance at the same time.
A modern headlamp assembly is not just a lamp. It is part optical device, part thermal system, and part regulatory item.
In ECE-regulated markets, approval depends on more than brightness. Beam control, marking accuracy, durability, and production consistency all matter.
This is why the headlight assembly ECE topic receives constant attention across AEVS coverage. Exterior design, smart optics, and compliance risk are now tightly linked.
For teams managing release gates, the practical question is simple: can this assembly legally ship, perform reliably, and survive audit review without surprises?
When people say “headlight assembly ECE,” what are they actually referring to?
In plain terms, headlight assembly ECE refers to the approval framework used in countries applying UNECE vehicle regulations.
The requirement usually covers the complete lamp assembly, not just the light source or housing in isolation.
Depending on technology, relevant regulations may include ECE R48 for installation, plus lamp-specific rules such as R112, R123, R149, or related EMC and environmental requirements.
That is where confusion often begins. A lens may look identical across regions, while the approved beam pattern and markings are completely different.
For LED headlight assemblies, the focus is usually on three linked questions:
- Is the optical performance compliant under the correct ECE regulation?
- Are the approval marks and functional identifiers correct on the product?
- Can volume production remain aligned with the approved type?
In actual programs, the third point causes many late issues. Approval is granted to a defined configuration, not to a general design intention.
Which marks on the lamp should be checked first?
If a shipment or sample needs a fast screening, start with the markings molded or engraved on the assembly.
The most recognized sign is the E-mark, shown as a capital “E” inside a circle with a number identifying the approving country.
That mark alone is not enough. It must match the approval number and the function codes relevant to the lamp design.
More common mistakes involve incomplete markings, wrong side designation, outdated function symbols, or marks copied from a previous variant.
A quick judgment table helps separate acceptable variation from real nonconformity.
When reviewing headlight assembly ECE documents, always compare the physical mark, drawing, certificate, and BOM together. One missing link is enough to stop release.
What tests usually determine whether approval will pass or fail?
Most failures do not come from a single dramatic defect. They come from marginal performance under formal test conditions.
Photometric testing is the center of the headlight assembly ECE process. The beam must hit required points and stay below glare limits.
For LED systems, thermal behavior matters because junction temperature can shift luminous output and beam stability during the test cycle.
In practice, the following checks are watched closely:
- Photometric distribution at specified measuring points.
- Color and chromaticity consistency where applicable.
- Vibration, dust, moisture, and sealing durability.
- Heat resistance of housing, lens, and internal components.
- Electrical compatibility with control units and vehicle systems.
- Mechanical aiming stability after endurance exposure.
For adaptive or matrix lighting, software logic and hardware response can also come under review, especially where anti-glare behavior depends on controlled switching.
This is where AEVS-style technical intelligence becomes useful. Optical algorithms, thermal models, and real operating loads should be reviewed together, not in separate silos.
How does the approval process usually unfold from sample to certificate?
The headlight assembly ECE pathway is usually shorter when variant control is tight from the beginning.
A common sequence looks like this.
- Define the exact lamp type, functions, light source architecture, and intended markets.
- Prepare technical drawings, marking layout, ratings, and component traceability records.
- Submit samples and documentation to the approval authority or technical service.
- Complete laboratory testing and address any nonconformity findings.
- Receive approval documentation and lock the approved configuration.
- Maintain Conformity of Production controls for ongoing manufacturing.
The final step is often underestimated. Conformity of Production is not a one-time form. It is the bridge between laboratory approval and shipping reality.
If a heat sink supplier changes, if LED binning shifts, or if lens material changes, the headlight assembly ECE status may need reassessment.
More often than expected, a “small engineering optimization” becomes a regulatory deviation.
Where do teams usually make the wrong call?
One frequent mistake is assuming that passing internal validation means ECE approval is secure. Internal standards may be tough, but they are not the same as regulatory acceptance.
Another mistake is treating headlight assembly ECE as a lamp-only issue. On current vehicles, aiming, installation height, control strategy, and sensor interaction can all affect compliance.
Several warning signs deserve early attention:
- Prototype samples differ from mass-production tooling.
- Marking artwork is approved late in the program.
- Optical simulations are not correlated with lab measurements.
- Software updates are released without regulatory impact review.
- Regional teams reuse DOT or local-market assumptions for ECE release.
Within the wider exterior system, those errors can also disturb styling intent, thermal packaging, and energy efficiency targets.
That is why AEVS often frames lighting as part of vehicle perception, not just a standalone commodity. The compliance decision sits inside a larger engineering chain.
What is a practical way to judge readiness before launch?
A useful readiness review blends document checks with physical verification. It should be done before final release, not after packaging is printed.
The table below works well as a short pre-launch screen for headlight assembly ECE status.
If two or more items fall into the escalate column, the program is not really launch-ready, even if sample performance looks acceptable.
A sound next step is to align the certificate set, test reports, marking drawings, and production controls into one release file.
That makes later audits easier and reduces confusion when platform changes affect lighting, sensors, wheels, or thermal packaging elsewhere on the vehicle exterior.
In short, headlight assembly ECE compliance is best managed as a controlled system decision. Review the marks, confirm the tests, lock the approved configuration, and keep production aligned with what was certified.
For the next review cycle, start with the highest-risk variants, especially adaptive LED assemblies used in NEV platforms, then map cost, timing, and regulatory gaps before release commitments are made.