
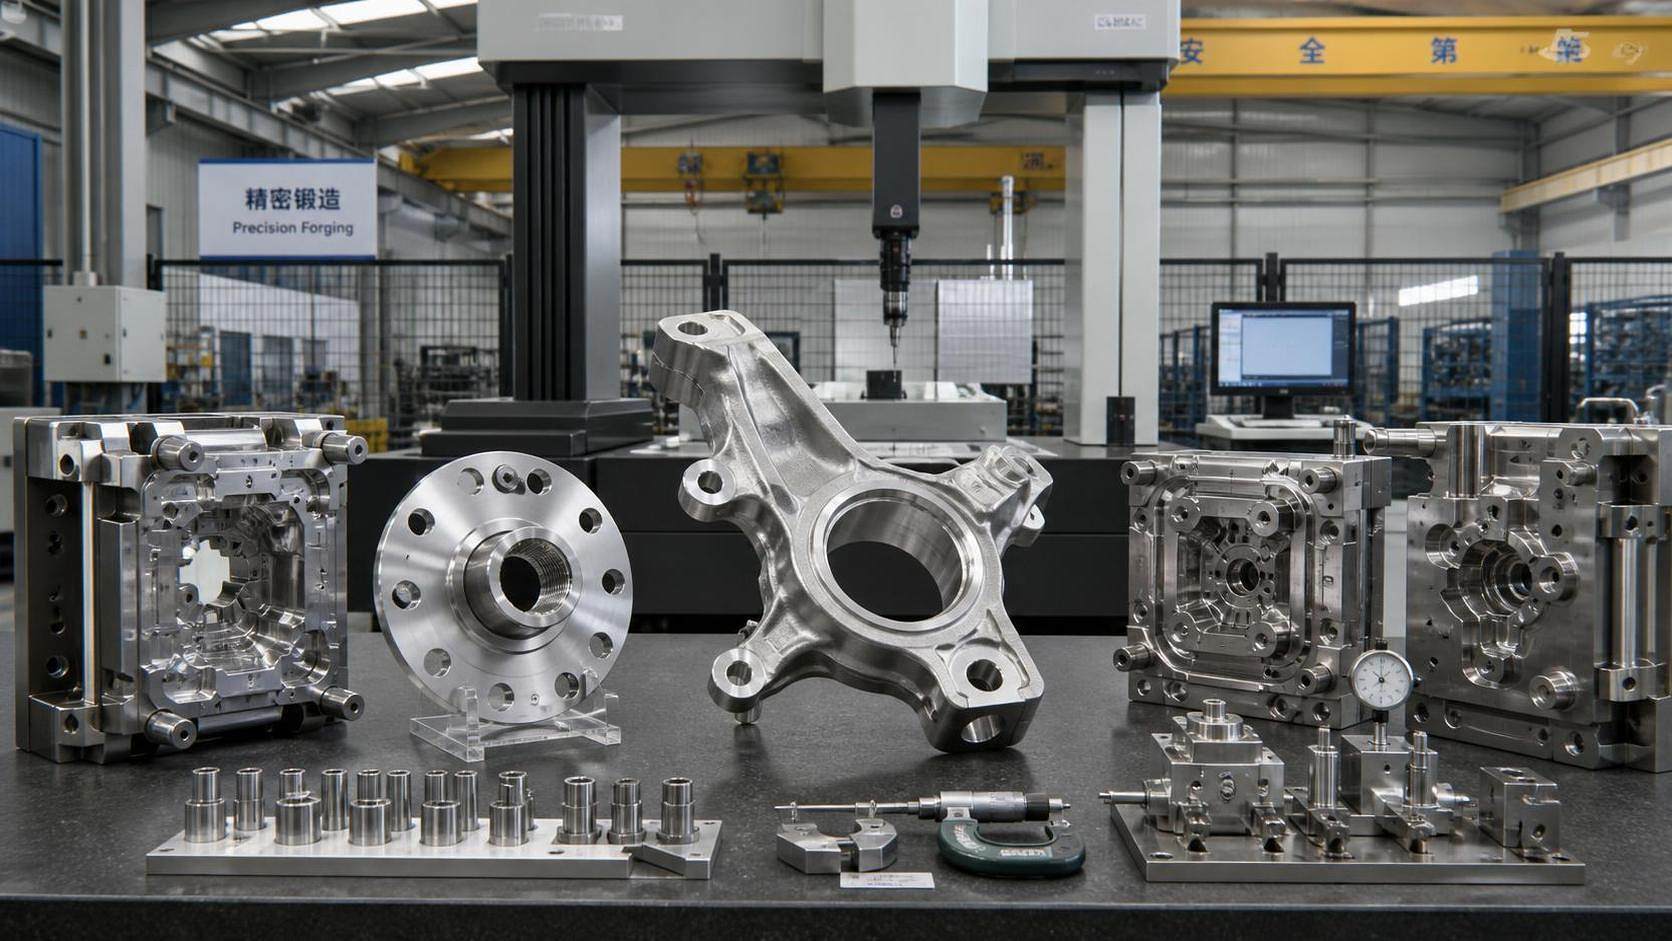
Supplier selection for complex forged auto parts usually fails on details that look minor during quotation review: grain flow direction, die life control, trim allowance, heat-treatment distortion, or whether dimensional capability is proven on the exact geometry rather than on a simple sample part. When the component will carry cyclic load, transfer steering input, support wheel-end mass, or hold tight sealing and mounting interfaces, a low quoted unit cost can quickly be offset by scrap, sorting, line stoppage, and repeated tooling correction. A reliable evaluation starts with the part itself: function, load path, tolerance stack, material grade, machining allowance, surface condition, and traceability depth.
A precision forging supplier should be assessed against the real manufacturing route needed for the part, not against a general claim of forging experience. A hub-related flange, suspension clevis, steering knuckle blank, high-strength bracket, or forged wheel center may all be called “complex auto parts,” yet they place very different demands on billet preparation, press tonnage, die design, flash control, trimming, straightening, heat treatment, shot blasting, machining datum strategy, and final inspection. The first useful question is whether the supplier has already produced parts with a similar material family, section-thickness variation, rib depth, boss geometry, and downstream machining burden.
Start with part criticality, not supplier brochures
Before comparing factories, define what failure would actually look like in your program. Some parts are sensitive to fatigue cracks at fillet transitions. Others are more vulnerable to bore ovality after quench, misalignment between forged features and machined datums, or inconsistent stock allowance that drives excessive machining time. If the drawing mixes tight geometric tolerances with difficult material behavior, the supplier should explain where the forging process ends and where machining process capability begins. Vague answers here usually mean the quotation was built from nominal dimensions rather than a full process review.
It is also worth separating parts that are “forged for strength” from parts that are “forged for material utilization and shape efficiency.” The evaluation criteria shift accordingly. A load-bearing exterior chassis-related component may need strict control of fiber flow and internal soundness. A lightweight wheel-related blank may put more pressure on weight consistency, surface integrity, and distortion control after thermal processing. If the application sits near braking heat, road salt, stone impact, or aggressive cleaning chemicals, ask how those conditions influenced the suggested alloy, coating interface, and residual stress strategy.
Read technical capability through process depth
A supplier that genuinely understands precision forging can walk through the process chain in engineering terms. The discussion should cover incoming bar or billet condition, cutoff method, heating window, descaling, preform sequence, blocker and finisher die logic, lubricant selection, press type, trimming plan, and how post-forging handling prevents bends, laps, folds, or scale entrapment. A capable plant will usually connect each process step to a known defect mode rather than treating production as a black box.
Material handling is one of the fastest ways to distinguish superficial capability from disciplined production. For alloy steel, microalloy steel, or aluminum alloy forgings, the supplier should be able to explain heat lot segregation, identification retention, and what happens when billets from different heats enter the same work order. If the answer relies on paper-only traceability without physical lot control on the shop floor, that is a practical risk. In complex auto parts, one mixed lot can complicate hardness results, machining response, coating adhesion, and failure analysis later.
Tooling competence matters just as much as press size. Precision forging depends on die design that respects material flow, venting, fillet radii, draft balance, wear concentration, and ejection behavior. Ask what internal simulation or review method is used before tooling release, how die corrections are approved, and whether tool steel selection changes with material type and production volume. A supplier that treats tooling as an external commodity may still deliver acceptable parts for low-complexity geometry, but repeated variation is more likely when the shape includes deep pockets, asymmetric bosses, or thin webs.
Quality systems should show control, not only certificates
Documents have limited value unless they are tied to operating discipline. In this segment, the stronger indicator is whether the factory can show how key characteristics are controlled in production: first-piece validation, in-process dimensional checks, die wear monitoring, furnace temperature records, hardness verification, and response steps when drift appears. Ask for examples of control plans or inspection reports with customer details removed. The content should show actual measurement logic, sampling rationale, reaction plans, and revision history.
For critical forged blanks, request clarity on destructive and non-destructive verification. Depending on part function, this may include macro-etch examination for flow lines, microstructure review, hardness mapping, ultrasonic inspection, magnetic particle testing, dye penetrant testing, or inclusion-related metallurgical checks. The right method depends on geometry and service condition. What matters during supplier evaluation is whether the plant knows which methods are meaningful for the part in question and where in the process they are most effective. A supplier offering every test without process context may be compensating for weak root-cause understanding.
Gauge management also deserves attention. Complex parts often fail because measurement strategy lags behind geometry complexity. If the supplier relies only on calipers and generic fixtures for parts with positional tolerances, compound angles, or critical bores, reported capability can look cleaner than actual fit in assembly. Ask whether they use CMM programs, attribute gauges tied to datums used in machining, and periodic correlation between shop-floor gauges and lab measurements.
Production consistency is often hidden behind sample success
One approved sample does not prove production readiness. The real test is whether the supplier can hold consistency across die life, heat-treatment batches, shifts, and maintenance intervals. Ask how many strokes or parts a die set typically runs before dimensional drift becomes material, how die wear is recorded, and what criteria trigger refurbishment. If the response is informal, expect variability in flash thickness, fill quality, parting-line shift, and machining stock.
Look closely at process capability on characteristics that are expensive to recover later. Excess stock on a forged surface may seem safe, yet it can extend cycle time, consume tools, and still leave warped geometry after rough machining. Too little stock creates a more direct problem: breakthrough, exposed laps, or inability to clean the surface. The right supplier should identify which dimensions are forged near-net, which are intentionally left with stable machining allowance, and how that allowance is verified in routine production.
Heat treatment often decides whether a promising forging source becomes a durable supply source. Distortion control, quench uniformity, hardness spread, and decarburization management are not interchangeable strengths across suppliers. If heat treatment is subcontracted, traceability and accountability need special attention. Ask where responsibility sits when forged dimensions are acceptable before heat treatment but fail after straightening or tempering. Ambiguity at this boundary tends to create disputes and delayed containment actions.
Cost evaluation should include the full conversion burden
A low forging quote may conceal cost transfer into machining, inspection, logistics, or warranty risk. Review the total conversion path: raw material yield, flash loss, expected machining removal, tool replacement frequency, heat-treatment routing, coating preparation, packaging protection, and transit-related deformation risk. A supplier with a higher piece price may still reduce total cost if the forging arrives with stable stock allowance, cleaner surfaces, better flatness, and more reliable lot discipline.
Freight and packaging deserve more scrutiny than they usually receive. Forged parts with protruding bosses, machined pilot surfaces, or narrow sealing lands can suffer edge damage, rust initiation, or part-to-part bruising if dunnage is weak. Export shipments add humidity exposure and longer dwell time. Ask how the supplier prevents corrosion after blasting or machining, how pallets are stacked, and whether lot identity remains visible after repacking. A quality plant that ships poorly can still become a chronic source of receiving and line-side problems.
Tooling ownership and maintenance terms should be read carefully during commercial review. Clarify who pays for initial dies, who approves engineering changes, what happens when annual volume differs from forecast, and whether spare die sets are included. For long programs, the hidden cost is often in repeated corrections, emergency refurbishment, or delayed replacement after die cracking. Commercial terms should reflect technical reality, especially when the geometry is unforgiving.
Audit the communication path as much as the equipment list
Complex forged parts rarely move smoothly when quoting, tooling, forging, heat treatment, machining, and quality are isolated from each other. During evaluation, notice whether the supplier can bring process engineers, quality staff, and production management into the same technical discussion. Questions about datum transfer, burr control, trimming distortion, or machining alignment should not bounce between departments without ownership. Strong communication during supplier assessment usually predicts faster containment when problems emerge in launch or serial production.
Engineering change handling is another practical filter. In vehicle exterior and chassis-adjacent applications, small design changes can alter forging feasibility more than expected. A radius reduction, wall thinning, or feature relocation may require new preform logic or different trimming support. Ask how changes are reviewed, how revision status is locked on the shop floor, and how mixed stock is prevented during transition. If the process depends on manual memory rather than a controlled release method, the risk is immediate.
Warning signs that are easy to miss
- A supplier emphasizes installed press tonnage but avoids discussing preform design, die wear pattern, or post-forging dimensional control.
- Inspection records look polished, yet there is no clear link between measured characteristics and the actual function of the part.
- Material certificates are available, but lot identity becomes hard to trace once billets are cut, heated, and moved into work-in-process containers.
- Quoted lead time appears short only because heat treatment, machining, or special inspection is expected to be outsourced without a defined control interface.
- Trial samples were produced under protected conditions that do not represent normal shift production, standard die age, or routine packing methods.
When comparing candidates, the most useful outcome is not a generic ranking but a process-specific risk map. One supplier may have stronger metallurgical discipline but weaker machining integration. Another may offer excellent forging geometry control while depending on less stable external heat treatment. A third may be competitive only if tolerances are relaxed or if rough machining is transferred upstream. That level of distinction is far more actionable than broad labels such as “qualified” or “preferred.”
A precision forging supplier earns confidence when technical explanations remain consistent from quotation through audit, sample development, and serial production planning. If the process story changes at each stage, cost and timing assumptions are probably unstable as well. For complex auto parts, the right source is usually the one that exposes process constraints early, defines controllable parameters clearly, and leaves fewer unknowns between forged blank and installed component.