
Industry Portal
Related News
- 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions
Vehicle Lightweighting Die Casting vs Stamping: Which Fits High-Volume Parts Better?
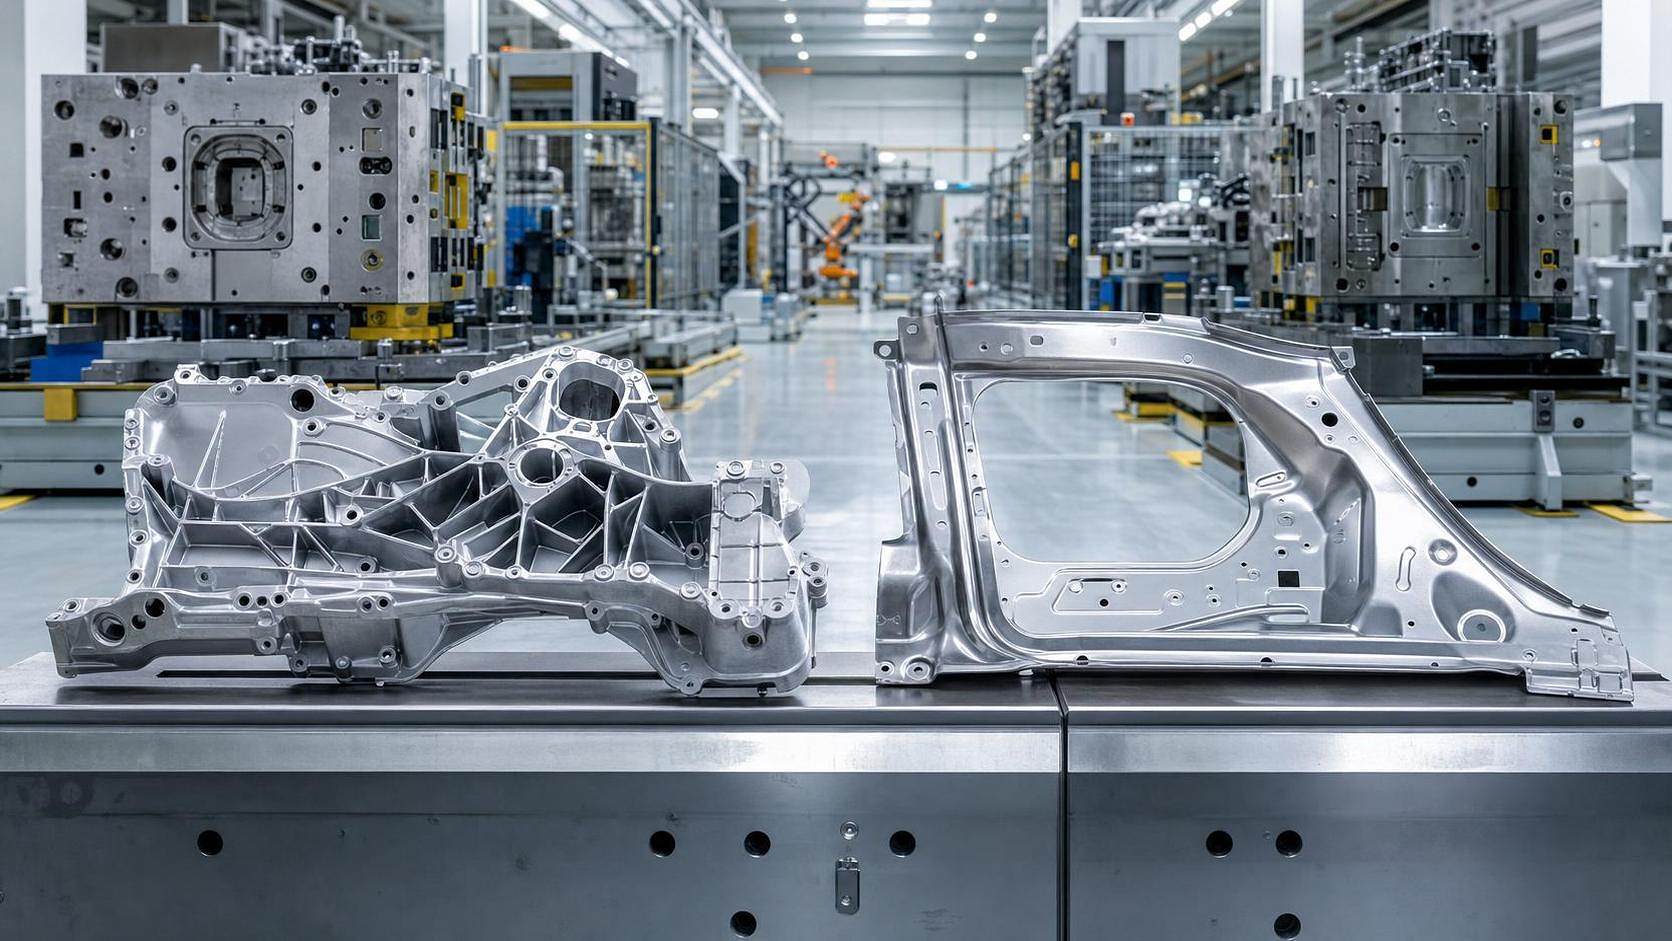
For high-volume vehicle programs, the debate around die casting and stamping is no longer a narrow process choice. It sits at the center of cost control, lightweight targets, structural performance, and launch timing. In that context, vehicle lightweighting die casting has gained attention because it can consolidate parts, reduce joining steps, and support complex geometries. Stamping, however, still holds a strong position where takt time, material utilization, and mature supply chains matter most.
The real question is not which process is universally better. It is which process fits a specific part family, production volume, alloy strategy, and downstream assembly logic. That is especially relevant in EV exterior and body-related systems, where every kilogram affects range, dynamics, and packaging.
Why this comparison matters now
Vehicle architectures are changing quickly. Battery packs add mass, crash structures must do more, and exterior systems increasingly combine aesthetics, aerodynamics, sensing, and structural duty.
That shift is visible across the AEVS focus areas. Lightweight wheel systems, headlamp packaging, sensor integration, roof modules, and airflow-sensitive exterior components all depend on manufacturing routes that balance form freedom with stable output.
In practical terms, vehicle lightweighting die casting becomes attractive when the part must integrate ribs, bosses, mounts, and functional interfaces in one shot. Stamping remains compelling when a thinner-gauge metal part can meet stiffness targets with simpler geometry and lower piece cost.
Two processes, two manufacturing logics
Die casting injects molten metal into a steel die under pressure. It is commonly used for aluminum and magnesium parts where dimensional repeatability and shape complexity are important.
Stamping forms sheet metal through a sequence of dies. It excels at high-speed production of panels, brackets, reinforcements, and shells with predictable thickness and strong process familiarity.
This difference creates a basic tradeoff. Vehicle lightweighting die casting offers integration and geometry freedom. Stamping offers speed, thinner sections, and broad manufacturing maturity.
Where die casting changes the equation
A cast part can replace several stamped pieces plus welds, fasteners, and fixtures. That changes not only part count, but also tolerance stack-up, assembly time, and logistics complexity.
In vehicle lightweighting die casting, weight reduction often comes from part integration rather than raw material reduction alone. A heavier local wall may still produce a lighter system.
Why stamping still dominates many high-volume programs
Stamping lines can run very fast. Tooling ecosystems are established, suppliers are abundant, and material behavior is well understood across automotive grades.
For large skin panels or relatively simple reinforcements, stamped steel or aluminum often remains the lowest-risk solution. The process is easier to scale across plants and platforms.
High-volume parts do not all reward the same choice
The phrase high-volume parts can be misleading. A million simple brackets and a million integrated structural nodes do not create the same manufacturing decision.
This is why vehicle lightweighting die casting tends to outperform stamping in cross-car beams, structural housings, brackets with integrated interfaces, and some EV platform nodes. Stamping usually stays ahead in closures, shields, covers, and broad sheet-based structures.
What technical evaluation should focus on
A clean comparison starts with the full system, not the isolated part drawing. Piece price alone often hides assembly labor, joining equipment, scrap handling, and warranty exposure.
- Check whether part integration reduces fixtures, welds, rivets, adhesives, or sealing steps.
- Compare dimensional stability after trimming, machining, coating, and thermal cycling.
- Review alloy availability, regional sourcing, and raw material volatility, especially for aluminum.
- Model scrap, rework, porosity risk, and die maintenance under actual production cadence.
- Include downstream functions such as sensor placement, airflow paths, and optical alignment needs.
That last point matters more than before. In AEVS-linked applications, exterior components increasingly support cameras, radar covers, lighting modules, and aerodynamic features. A manufacturing route that simplifies those interfaces may create value beyond mass reduction.
Performance, quality, and hidden risks
Vehicle lightweighting die casting can deliver strong stiffness-to-function outcomes, but quality control must be disciplined. Porosity, thermal distortion, and local property variation can become critical if the part also carries structural or sealing duties.
Stamping has its own limits. Springback, tool wear, crack sensitivity in complex forms, and multi-step joining can reduce theoretical simplicity. In some cases, the stamped solution only appears cheaper before assembly costs are counted.
For exterior systems, appearance and tolerance matter as much as strength. A headlamp carrier, roof frame support, or sensor bracket may fail commercially because of fit and alignment drift, not because of structural collapse.
Compliance and lifecycle pressure
ECE and DOT requirements, corrosion expectations, recyclability targets, and decarbonization reporting all influence process selection. These factors increasingly shape sourcing decisions alongside engineering metrics.
AEVS tracks exactly these cross-signals: regulatory shifts, aluminum price movement, optical packaging trends, and thermal or airflow performance. That broader view is useful because the process choice rarely stays confined to manufacturing engineering.
Typical use cases in exterior and adjacent systems
The most suitable process often depends on how many functions the part must absorb.
- Die casting fits integrated lamp brackets, wheel-adjacent structural supports, roof module frames, and sensor mounting carriers.
- Stamping fits shields, simple reinforcement panels, closure inners, and thin-gauge brackets with modest geometry.
- Hybrid solutions fit mixed-load assemblies, where stamped shells combine with cast nodes or local cast reinforcements.
This hybrid path deserves attention. Many programs do not need a total shift from sheet metal to cast architecture. A targeted use of vehicle lightweighting die casting around high-complexity zones can produce better economics than a full redesign.
How to make the decision more reliable
A useful evaluation framework should compare at least five things at once: mass, piece cost, tooling cost, assembly simplification, and quality stability over volume ramp.
When those questions are answered together, the die casting versus stamping debate becomes much clearer. The strongest answer often emerges from total system economics, not from a single process metric.
A practical reading of the market
Vehicle lightweighting die casting is likely to expand in EV platforms, especially where integration, packaging density, and module consolidation drive value. Stamping will remain indispensable for many high-volume parts because it is fast, proven, and highly efficient in the right geometry band.
The most realistic strategy is selective adoption. Use casting where functional integration changes the economics. Keep stamping where thin sheet architecture already performs well. In mixed exterior and vision-related systems, that balanced approach often produces the best manufacturing result.
The next step is to map candidate parts by geometry complexity, joining burden, tolerance sensitivity, and lightweight contribution. From there, compare vehicle lightweighting die casting and stamping at the assembly level, with material, compliance, and future platform requirements included from the start.