
Industry Portal
Related News
- 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions - 00
0000-00
Private Label Tire Export: Evaluating Suppliers, Compliance, and Landed Cost - 00
0000-00
DOT-Compliant Truck Lighting: A Practical Guide to FMVSS 108 Requirements
Low-Pressure Casting Explained: Best Materials, Process Steps, and Typical Defects
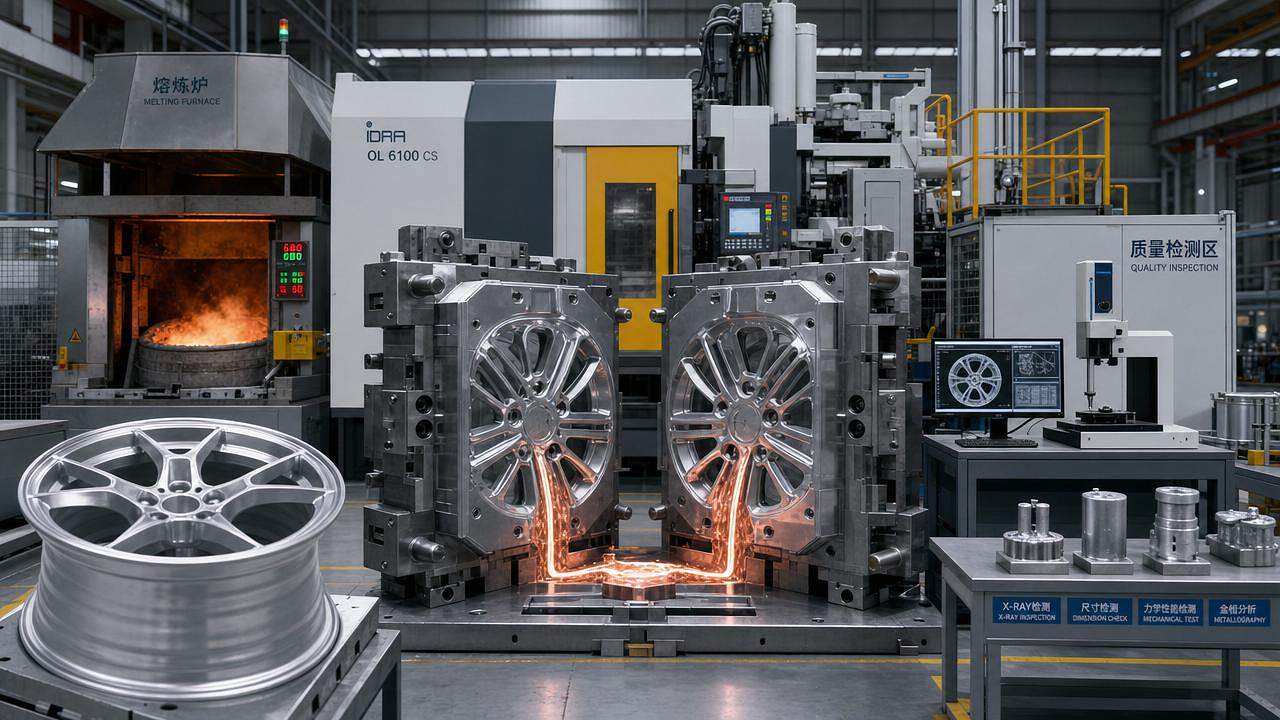
Low-pressure casting sits at the center of lightweight automotive manufacturing because it combines controlled metal flow, repeatable quality, and efficient material use. In wheel programs, suspension parts, and selected structural components, it supports the balance that matters most today: lower mass, stable strength, and fewer surprises in production.
That balance is especially relevant across the AEVS landscape, where aluminum wheels, aerodynamic efficiency, brake cooling, safety margins, and cost discipline all interact. A process choice is no longer only about shaping metal. It also affects vehicle range, visual quality, compliance, and how reliably a launch program stays on schedule.
Why low-pressure casting matters now
Electrified vehicles place unusual pressure on exterior and chassis-related components. Battery packs add weight. Instant torque raises load intensity. Customers also expect quieter driving, refined appearance, and durable performance under demanding road conditions.
In that context, low-pressure casting becomes more than a foundry method. It is a manufacturing strategy for producing aluminum parts with better density and tighter dimensional consistency than many conventional gravity methods.
For AEVS-relevant categories, aluminum alloy wheels are the clearest example. Wheel design must satisfy styling, airflow, impact resistance, fatigue life, and weight targets at the same time. A stable casting route helps align those objectives early, before quality issues migrate into machining, coating, validation, or field performance.
A practical definition of the process
Low-pressure casting uses gas pressure to push molten metal upward from a sealed furnace into a die. The filling motion is smooth and controlled, rather than fast and turbulent.
Because the metal enters from below, the process can reduce oxide formation, air entrapment, and random flow behavior. Directional solidification is also easier to manage. This matters when porosity limits structural performance or later heat treatment response.
Simple parts may be produced by other methods at lower tooling cost. But when surface quality, mechanical reliability, and repeatability matter, low-pressure casting often becomes the preferred choice.
Best materials for low-pressure casting
The most common materials are aluminum alloys, especially where low mass and corrosion resistance are required. Material selection should reflect not only final strength, but also castability, heat treatment behavior, and scrap sensitivity.
Common alloy options
In practice, A356 remains the benchmark for low-pressure casting in aluminum wheels. It offers a reliable mix of process stability, mechanical strength, and commercial availability.
Material choice should also consider regional standards, recycling content, and raw metal fluctuation. For global programs, that commercial layer matters almost as much as metallurgical performance.
What deserves closer attention
- Iron content, because excess iron can reduce ductility.
- Hydrogen control, because dissolved gas drives porosity.
- Modification and grain refinement, which shape microstructure and fatigue behavior.
- Heat treatment compatibility, especially when T6 properties are required.
Core process steps and where risk begins
A typical low-pressure casting line looks straightforward from a distance. Actual performance depends on how tightly each step connects to the next.
1. Melt preparation
This stage sets the baseline. Alloy chemistry, melt cleanliness, degassing quality, and holding temperature directly affect internal soundness. Poor melt preparation cannot be fully corrected later.
2. Die preparation
The die must reach the right thermal condition before pouring. Uneven die temperature creates unstable filling, local shrinkage, and surface marks. Coating application also influences release behavior and local heat transfer.
3. Pressurized filling
Gas pressure pushes molten aluminum upward through a riser tube. Pressure rise speed matters. Too fast invites turbulence. Too slow can create cold shuts or incomplete filling in thin sections.
4. Solidification control
This is where the process earns its reputation. Controlled pressure can continue feeding metal during solidification, helping reduce shrinkage porosity. Cooling layout, die temperature zones, and section thickness determine whether that advantage is realized.
5. Ejection, finishing, and heat treatment
After removal, castings move into trimming, inspection, machining, and often T5 or T6 treatment. If porosity or segregation is already present, later operations usually expose it rather than solve it.
Typical defects in low-pressure casting
Most defects in low-pressure casting are not random. They are linked to a specific mismatch between material condition, thermal balance, die design, and pressure curve.
Wheel programs often feel these defects quickly because X-ray inspection, machining exposure, and fatigue testing make hidden weaknesses visible. That is why low-pressure casting control should be built into launch planning, not treated as a late-stage quality gate.
How the process connects to business decisions
The value of low-pressure casting is not limited to metallurgical quality. It influences tooling strategy, cycle time, scrap rate, certification confidence, and supplier readiness.
For AEVS-linked applications, this is especially important where wheel aerodynamics, brake airflow, coating appearance, and road load durability must align. A casting route that produces stable geometry reduces downstream correction work in machining and balancing.
It also supports broader decarbonization goals. Better yield and lower rework mean less wasted material and less hidden energy consumption across melting, heat treatment, and finishing.
Where low-pressure casting fits best
Not every part should use this method. The strongest fit appears when the component needs a combination of shape complexity, attractive surface finish, and dependable mechanical behavior.
- Aluminum alloy wheels for passenger cars, SUVs, and EV platforms.
- Suspension and chassis-related castings where fatigue life matters.
- Selected housings and support structures requiring low porosity.
- Programs where appearance and dimensional repeatability carry commercial value.
If wall sections are extremely thin or production economics favor another route, high-pressure die casting or forging may be more suitable. The right answer depends on total program requirements, not on process preference alone.
Useful checkpoints before committing
A stronger decision usually comes from comparing process capability against part function, rather than focusing only on piece price.
- Confirm whether the alloy and heat treatment route match fatigue and impact targets.
- Review simulation for fill pattern, hot spots, and feeding behavior.
- Check inspection strategy, especially X-ray criteria and destructive validation timing.
- Evaluate scrap assumptions, not only nominal cycle time.
- Link casting quality to downstream machining, coating, and balance performance.
- Watch raw aluminum price movement and regional compliance requirements.
Low-pressure casting remains one of the most practical routes for high-value aluminum components, especially where lightweight design and reliability must coexist. The main question is rarely whether the process works. It is whether materials, tooling, thermal control, and defect prevention have been aligned early enough.
That makes the next step fairly clear. Define the performance window, map the likely defect risks, and compare supplier capability against actual program priorities. From there, low-pressure casting becomes easier to judge as a long-term manufacturing decision, not just a production method.