Industry Portal
Related News
- 00
0000-00
NEV Industry Standards in China: Which Battery Safety Tests Are Required? - 00
0000-00
Automotive Exterior Lighting Systems: Lamp Types, Functions, and Placement - 00
0000-00
Choosing an Electric SUV Sunroof: Key Fit, Safety, and Weather-Sealing Factors - 00
0000-00
Pop-Up Automotive Sunroof Systems: Key Design Factors for Vehicle Integration - 00
0000-00
Automotive Product Comparison Charts: How Buyers Can Compare Specs, Cost, and Fit
ISO 9001 Requirements for Automotive Exterior Component Suppliers
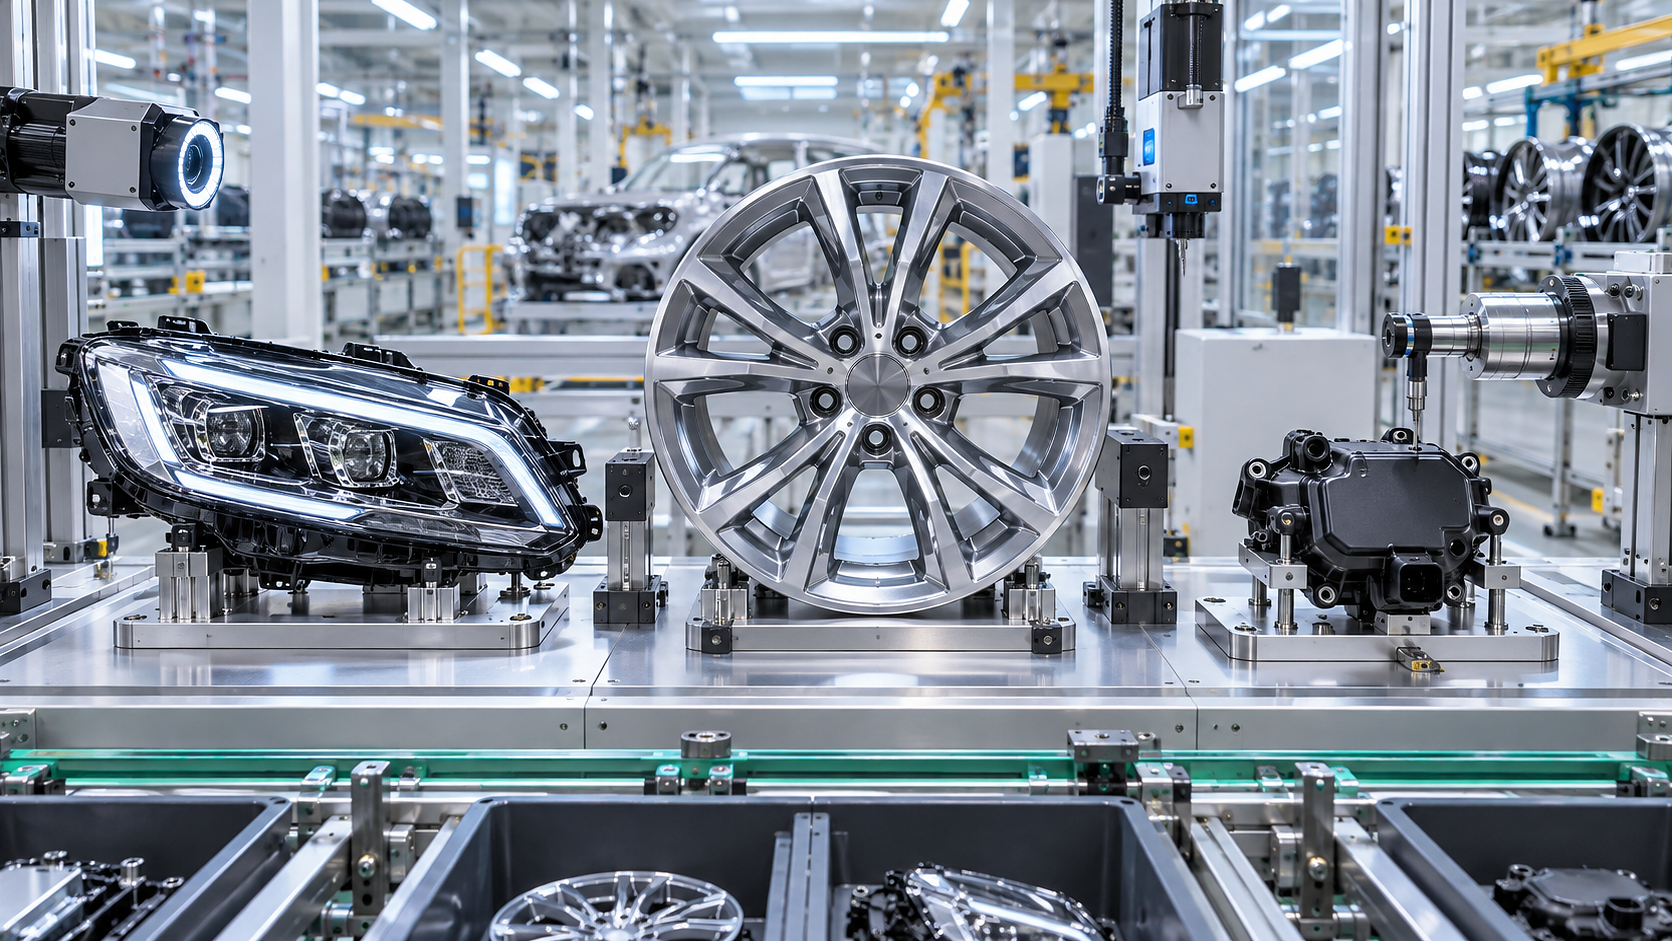
ISO 9001 requirements for automotive exterior component suppliers begin with control of the processes that create the part, not with inspection of the finished surface. A visually acceptable wheel, headlamp lens, roof module, sensor housing, or exterior trim part can still contain an uncontrolled material change, an unverified software configuration, a mixed production lot, or an incomplete release record. ISO 9001 requires a quality management system that makes these conditions visible, controlled, and traceable before they reach vehicle assembly or the aftermarket.
For exterior components, conformity has several layers. Dimensional fit, appearance, durability, functional performance, safety-related characteristics, packaging condition, and documented customer requirements must all align. The system must define how those requirements enter the organization, how they are translated into production controls, and how evidence of conformity is retained. A final inspection record alone is rarely enough evidence when a defect could have originated in incoming material, tooling condition, curing, assembly, calibration, or a change to a controlled document.
Start with the actual product requirements
ISO 9001 requires customer requirements to be reviewed before acceptance and controlled through the product realization process. For automotive exterior parts, this review should distinguish between requirements that look similar but demand different controls. A wheel’s cosmetic coating standard is not the same as its structural requirements. A headlamp’s lens appearance is separate from optical alignment, sealing integrity, thermal behavior, and traceability of electronic subassemblies. A sunroof system requires controls for glass, seals, drive mechanisms, drainage interfaces, noise behavior, and installation geometry.
Requirements should be converted into measurable specifications wherever possible. “No visible defects” is too broad unless the viewing distance, lighting condition, reference sample, defect category, and acceptance boundary are defined. “Correct fit” also needs a datum scheme, measurement method, fixture condition, permitted variation, and a clear understanding of whether the feature is checked as a component or after assembly with mating parts.
Some characteristics are easily misread when examined alone:
- A painted surface can meet gloss and color targets while showing poor adhesion after pretreatment variation or curing instability.
- A sensor switch can pass a bench functional test yet fail after connector stress, moisture exposure, vibration, or incorrect vehicle-network configuration.
- A forged or cast wheel can meet a dimensional drawing while retaining an unapproved alloy chemistry, porosity concern, or heat-treatment record gap.
- A headlamp assembly can be free of visible condensation at release but remain vulnerable if vent membranes, housing welds, gasket compression, or drying controls were not verified.
The review process should therefore identify product characteristics, special handling needs, test evidence, legal or regulatory obligations provided by the customer or applicable to the supplied market, and any required approval route for deviations. ISO 9001 does not prescribe a single automotive control-plan format, but the quality system needs a reliable connection between each requirement and the process control that protects it.
Process control must reflect how the component can fail
Clause 8 of ISO 9001 requires controlled conditions for production and service provision. In exterior-component production, this means work instructions, qualified equipment, suitable monitoring resources, competent personnel, defined release criteria, and prevention of human error where practical. The depth of control should follow the consequence and detectability of a failure.
For aluminum alloy wheels, incoming alloy identification, melt control, casting or forging parameters, heat treatment, machining, surface preparation, coating cure, runout measurement, and marking all influence conformity. A defect discovered after coating may be difficult to link back to the relevant melt, mold condition, or heat-treatment batch if traceability is limited to the final paint lot. The process route should preserve the identity of the lot through the stages where the material and structure can change.
For LED headlamp assemblies, critical variation may originate at optical components, LED boards, heat sinks, adhesives, welded housings, aiming features, and embedded electronics. The same appearance defect can have different causes: haze in a lens can arise from material handling, molding parameters, protective-film residue, chemical contamination, or internal outgassing. Treating all haze as a cleaning issue delays effective corrective action. The process must capture the evidence needed to separate these causes.
Sunroof systems require particular attention to interfaces. Rail alignment, glass bonding, seal placement, motor and cable operation, drain routing, and torque-controlled fasteners may each be individually acceptable while the completed module binds, leaks, rattles, or does not seat correctly in the roof opening. Controls should include the assembly sequence and interaction of features, not only isolated component measurements.
Exterior sensor switches and related housings introduce a different combination of risks. Protection against ingress, connector retention, sealing surfaces, firmware or configuration identity, sensor orientation, and test coverage need coherent control. A passed end-of-line electrical test does not prove that the installed orientation or software version is correct. Identification and release records must allow the supplied unit to be associated with the approved configuration.
Documented information must be usable on the shop floor
ISO 9001 requires documented information to be controlled so that the current approved version is available where it is needed and obsolete versions are prevented from unintended use. In automotive exterior production, unclear document control often appears as a mismatch between engineering intent and production practice: a revised torque value is absent from the station instruction, an old appearance standard remains at the inspection point, or a revised packaging method is not reflected in shipping documentation.
Documents should state enough detail to support repeatable work. A broad instruction to “inspect seal condition” leaves room for inconsistent interpretation. A better controlled instruction identifies the applicable seal, inspection location, lighting or magnification conditions where relevant, permitted condition, response to a suspect finding, and required record. The purpose is not excessive paperwork. It is preventing individual judgment from replacing a defined acceptance method.
Electronic records require the same discipline. Measurement files, test-program revisions, calibration status, inspection images, nonconformance records, and release data should be protected against unintended alteration and retrievable for the defined retention period. When data are used to release a batch, the record must identify the product, relevant lot or serial range, date, result, and person or authorized function responsible for release.
Traceability should follow risk, not convenience
ISO 9001 requires identification of outputs where necessary and traceability when it is a requirement. Automotive exterior components often require more than a shipping label because failures may emerge after environmental exposure, installation, or vehicle use. The traceability model should make it possible to determine what material, production period, process route, inspection status, and configuration apply to a supplied unit or lot.
The appropriate unit of traceability differs by product. A decorative trim part produced in a stable molding run may use lot-level traceability if the customer requirement and risk assessment support it. A safety-relevant wheel, a complex lighting assembly, or an electronic sensor module may require tighter linkage between the finished component and its critical material, process, and test evidence. The system should not assume that one traceability level fits every part family.
Physical marking must remain readable without damaging function or appearance. Where direct marking is unsuitable, packaging labels and controlled batch segregation may be used, provided the association cannot be lost during rework, temporary storage, or partial shipment. Repackaging is a frequent weak point: once an original container is opened, lot identity, quantity reconciliation, and inspection status can become uncertain unless the process explicitly preserves them.
Control externally provided processes and materials
ISO 9001 requires external providers to be evaluated, selected, monitored, and re-evaluated according to their ability to meet requirements. For exterior components, the external scope may include castings, forgings, coatings, lenses, electronic boards, seals, adhesives, plating, laboratory testing, packaging, and transport. Approval should address the supplied item’s effect on the final component rather than rely only on a general supplier questionnaire.
A material certificate does not remove the need for incoming control when the material’s condition can change in transport or storage. Adhesives and sealants may be affected by shelf-life management, temperature exposure, mixing ratio, or moisture. Polymeric optical materials can be damaged by handling, contamination, or incorrect drying. Coated decorative parts need protection from abrasion and chemical contact. Incoming verification should be proportionate to the risk and should include the identity, condition, documentation, and any critical properties that cannot be reliably detected later.
External laboratory results also need evaluation. The report must relate to the correct sample, revision, method, test condition, and acceptance criterion. A favorable result is not transferable to a revised design, altered material source, or changed process unless the technical basis for that transfer has been reviewed.
Measurement systems need control before their results are trusted
Monitoring and measuring resources must be suitable for their intended purpose and maintained so that results remain valid. This covers gauges, torque tools, optical measurement equipment, test rigs, leak-test devices, electrical test stations, software-controlled testers, and visual inspection conditions. Calibration labels alone do not demonstrate that a system can distinguish acceptable from unacceptable product at the required tolerance.
Fixture wear is particularly important for complex exterior geometries. A fixture may repeatedly produce stable readings while locating the part incorrectly because pins, nests, clamps, or reference surfaces have worn. The resulting data can look consistent but be wrong. Verification should consider the fixture’s relationship to product datums, not only the instrument mounted on it.
Visual inspection needs controlled lighting, approved boundary samples where used, and a defined inspection sequence. Without those conditions, inspectors may reach different decisions on sink marks, flow lines, orange peel, particles, gloss variation, scratches, or lens defects. Aesthetic requirements are subjective only when the acceptance criteria are left undefined.
Nonconforming output requires containment and a reasoned disposition
When nonconforming output is found, ISO 9001 requires it to be identified and controlled to prevent unintended use or delivery. The affected product should be segregated or electronically blocked as appropriate, and the system must preserve evidence of the nonconformity, decision, and authorization. Rework requires defined instructions and re-verification against the applicable requirements before release.
Disposition decisions need technical context. Re-polishing a wheel surface may correct a cosmetic issue but alter a protective layer or dimensional surface. Reheating a bonded headlamp assembly may affect optical parts, seals, or electronic components. Rework on a sensor housing can solve flash or burr concerns while compromising a sealing interface. The release decision must address all characteristics potentially affected by the rework, rather than only the original defect.
Customer concessions, when permitted by the applicable agreement, should be controlled as time-bound and quantity-bound exceptions. A concession is not evidence that the underlying process has become acceptable. Repeated requests for the same concession indicate that corrective action has not removed the source of variation.
Corrective action should test the cause, not merely close the record
ISO 9001 expects nonconformities to be addressed, causes evaluated, corrective actions implemented, and effectiveness reviewed. A useful investigation separates the observed defect from the mechanism that produced it. For example, water ingress in a lighting assembly could relate to damaged seals, uneven gasket compression, poor weld parameters, blocked venting, housing distortion, incorrect assembly sequence, or test-method limitations. Replacing the seal may reduce immediate rejects while leaving the actual mechanism unchanged.
Evidence for root-cause analysis should include product and process history: affected lot range, shift, machine state, tooling condition, material batch, operator sequence where relevant, environmental conditions, inspection data, maintenance activity, and prior deviations. The aim is to establish why the existing controls did not prevent or detect the issue. Corrective action is stronger when it changes the control point, acceptance method, mistake-proofing feature, maintenance trigger, or training content that allowed the failure to escape.
Management review, internal audits, performance evaluation, and continual improvement complete the ISO 9001 system. Their value lies in testing whether process data, complaints, audit findings, rework patterns, supplier issues, and delivery records reveal a recurring weakness. For automotive exterior components, a controlled process is one that can show how each critical requirement was understood, protected, verified, released, and investigated when performance departed from expectation.