
Industry Portal
Related News
- 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions
How to Select Automotive Exterior Door Garnish for Durability, Fit, and Finish
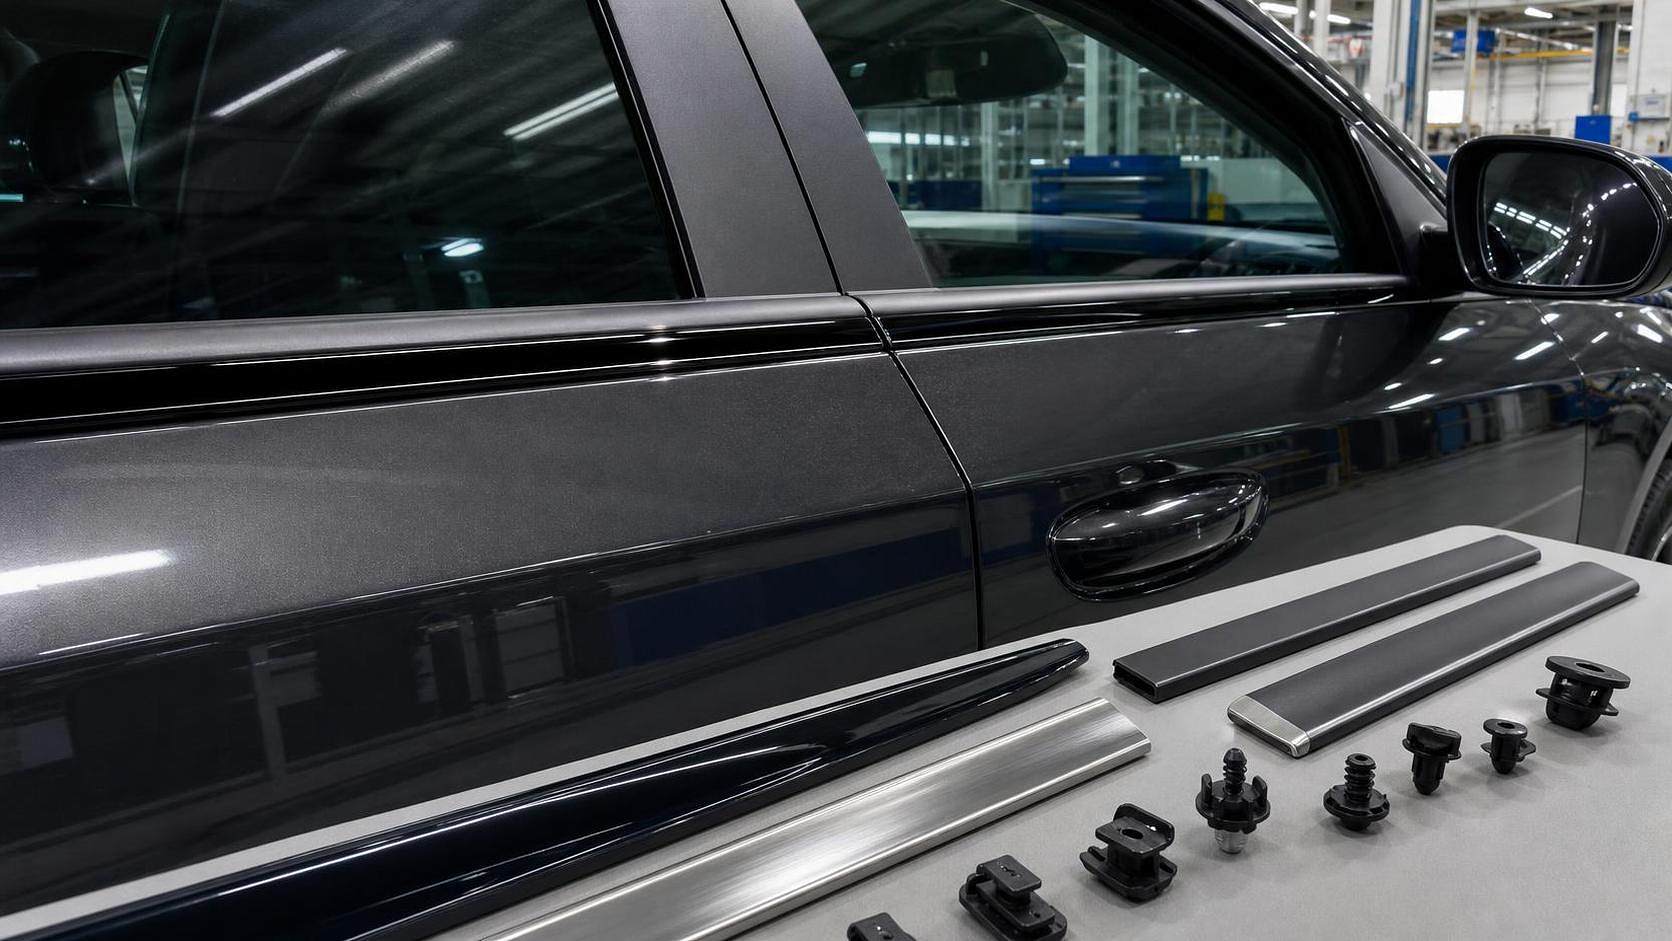
Selecting the right automotive exterior components door garnish is not just a styling decision—it directly affects long-term durability, installation accuracy, and surface finish consistency. For technical evaluators, the challenge lies in balancing material performance, dimensional fit, weather resistance, and manufacturing quality. This guide outlines the key criteria that help identify door garnish solutions capable of meeting both vehicle appearance standards and demanding real-world operating conditions.
In many sourcing discussions, door garnish is still treated as a low-complexity trim part. That assumption usually fails once the program enters validation or field use. Exterior garnish sits in a difficult position: it must maintain visual quality under constant UV exposure, heat cycling, moisture, road debris, detergents, and assembly variation, while also aligning precisely with adjacent sheet metal, glass, beltline trim, seals, and sometimes camera or sensor-related exterior architecture. A garnish that looks acceptable at PPAP can still become a warranty issue if gloss shift, edge lift, clip breakage, sink marks, or color mismatch appear six to eighteen months later.
For that reason, technical evaluation should not begin with appearance samples alone. It should begin with a more practical question: what failure modes can the part realistically survive in the target vehicle environment, and what process capability does the supplier have to control those risks at scale?
Why door garnish selection is more demanding than it appears
Door garnish often combines styling, aerodynamic contour, and brand identity in a thin exterior component with tight visual tolerances. Depending on the vehicle architecture, it may be positioned along the window frame, beltline, pillar area, lower door section, or protective side trim zone. In each case, its performance expectations differ.
A gloss black window surround garnish on a premium EV, for example, faces different risks than a textured lower side door garnish on a commercial vehicle. The first will be judged mainly on surface finish, waviness control, scratch visibility, and fit-to-body precision. The second may be judged more on stone-chip resistance, retention strength, dimensional stability, and impact tolerance. Treating both as equivalent “plastic exterior trim” leads to weak specifications and supplier misalignment.
The technical review should therefore separate three performance layers:
- Structural and dimensional reliability
- Environmental durability
- Visual finish stability over time
Only after these are defined clearly does material and process selection become meaningful.
Start with the substrate: material choice determines most downstream risk
Material selection is the most important early decision because it affects thermal expansion, paintability, impact behavior, clip integrity, gloss retention, and cost structure. Common substrate options in door garnish programs include ABS, ASA, PC/ABS, PP-based compounds, and engineering plastics with mineral or glass reinforcement. In some applications, stainless steel or aluminum decorative trims are also used, but polymer systems dominate where lightweighting, shape flexibility, and cost efficiency matter.
ABS is often selected for good moldability and acceptable surface quality, but its outdoor weatherability is limited unless protected through coating or film solutions. ASA offers better UV resistance and color stability for exposed applications, especially in molded-in-color parts. PC/ABS can help where dimensional precision and impact performance are needed, though weather resistance still depends on grade selection and surface treatment strategy. PP compounds can be attractive for cost and weight, but their lower surface energy and dimensional behavior may complicate finishing and class-A appearance requirements.
The evaluator should not ask only “What resin is used?” but rather:
- Is the resin grade automotive exterior qualified for long-term UV exposure?
- What is the coefficient of thermal expansion relative to the mounting structure?
- How does the material behave at low-temperature impact conditions?
- Does it support the required paint, film, plating, or hard-coat system reliably?
- How sensitive is it to molding shrink variation across long and thin geometries?
One common error is approving a visually good sample made from a material grade that performs acceptably in lab appearance checks but lacks proven outdoor stability in aggressive climates. Door garnish on vehicles shipped across the Middle East, Southeast Asia, North America, and Europe must tolerate very different heat loads, UV intensity, humidity, and winter chemical exposure. A technically sound selection must reflect the actual export market mix, not only the development center’s local validation assumptions.
Durability is not a single test result
Suppliers often present durability confidence through a short list of passed tests. That is useful, but not sufficient. Door garnish durability should be assessed as a failure chain rather than a checklist. A part may pass isolated UV exposure yet still fail in service because thermal cycling weakens the bond line, water ingress affects retention clips, or car-wash abrasion rapidly degrades a piano black surface.
The most relevant durability dimensions usually include:
- UV and weathering resistance
- Heat aging and thermal cycling
- Humidity and water resistance
- Chemical resistance to detergents, waxes, de-icing agents, and fuels where relevant
- Stone-chip and scratch resistance
- Retention performance after repeated expansion and contraction
For technical evaluation, the key is correlation. Which validation methods best correlate with actual field failure in the intended vehicle segment? In premium passenger vehicles, appearance degradation may trigger rejection before structural failure occurs. In fleet or utility vehicles, clip retention loss or local warpage may matter more than micro-scratch visibility.
Accelerated weathering standards and OEM-specific test protocols vary, and the exact test matrix is usually program dependent. Where a supplier cites “UV passed” without protocol details, exposure duration, gloss delta, color shift, or post-aging mechanical retention data, the result should be treated as incomplete. Exterior trim durability is highly dependent on both material system and process quality, especially for coated or laminated parts.
Fit is a system issue, not only a tooling issue
Poor fit is often blamed on mold accuracy, but in practice it is a system-level issue involving part design, substrate behavior, attachment strategy, body tolerance stack-up, and plant assembly conditions. Door garnish typically interfaces with door outer panels, channels, seals, clips, tapes, studs, or snap features. Even a well-molded part can show inconsistent gap and flush if the attachment concept does not accommodate thermal movement or door build variation.
Technical evaluation should focus on how the part behaves after assembly, not just on bench measurement. Important questions include:
- What is the allowable gap and flush window across the full vehicle tolerance stack?
- Is the part rigid enough to hold shape, but compliant enough to assemble without stress whitening or distortion?
- Do clips and locator features control position repeatably?
- Will double-sided adhesive systems maintain bond under heat, moisture, and surface contamination?
- How does the garnish behave when mounted on curved door surfaces with local variation?
Long, narrow garnish parts are especially vulnerable to warpage and assembly-induced stress. If the part requires forceful installation to meet visual alignment, residual stress can later appear as edge lift, squeak, localized deformation, or cracked fastening features. This is why digital nominal fit data should be supported by capability evidence from molded parts across multiple production batches, ideally with assembly simulation or trial builds.
For export-oriented programs, fit stability after logistics exposure also deserves more attention than it usually gets. Parts shipped in bulk across humid or hot transport routes can deform if packaging support is poor or residual molding stress is high. A technically capable supplier should be able to discuss packaging-induced deformation risk, not only molding tolerances.
Finish quality is where many programs underestimate risk
Surface finish issues are among the most visible and commercially damaging problems in exterior garnish. The challenge is that “good finish” means different things depending on design intent: textured matte, body-color painted, metallic-look, chrome-like, satin black, or high-gloss black all have different defect sensitivities.
Piano black and other glossy dark finishes deserve special caution. They can create a premium look, but they amplify even minor molding flow marks, sink, orange peel, particulate contamination, edge waviness, and assembly scratches. In field conditions, they also reveal wash-induced marring faster than many styling teams anticipate.
When assessing finish capability, the evaluator should examine not only a master sample under showroom lighting but also:
- Surface consistency under direct sunlight and low-angle light
- Part-to-part gloss variation across cavities and batches
- Edge quality and gate witness control
- Coating adhesion and chip resistance
- Scratch visibility after normal cleaning and assembly handling
- Color harmony with adjacent trims from different suppliers
This is particularly important when the automotive exterior components door garnish is sourced separately from mirror trim, pillar appliqués, beltline moldings, or other visual neighbors. A garnish may pass its own specification but still create an unacceptable vehicle-level appearance mismatch. Cross-component harmony is often where technically “compliant” parts fail in management reviews.
Attachment method can be the hidden weak point
Many door garnish failures are not substrate failures at all. They are attachment failures. The choice between clips, studs, tape, hybrid fastening, or overmolded attachment features directly affects assembly efficiency, serviceability, and long-term retention.
Clip-only designs can simplify service but may suffer from rattling, tolerance sensitivity, or localized stress. Tape-only solutions can improve appearance by avoiding sink around fasteners, yet they depend heavily on surface preparation, adhesive selection, and environmental resistance. Hybrid approaches often provide better security, but they also increase process complexity.
Questions worth asking during selection include:
- What is the retention margin after aging, not just initial pull-off strength?
- How robust is installation in plant conditions with dust, humidity, and operator variation?
- Can the part be removed for service without damaging paint or adjacent trim?
- Are clip materials and geometry matched to repeated thermal cycling?
- Is galvanic or corrosion interaction relevant if metal inserts or studs are used?
In aftermarket and replacement channels, attachment robustness becomes even more important because field installation quality is less controlled than OEM line installation. Parts that are technically acceptable in factory assembly can create high complaint rates when distributed through service or independent repair networks.
Manufacturing process capability matters as much as design intent
In supplier comparison, it is easy to overvalue CAD, prototype quality, and presentation quality while undervaluing process discipline. Door garnish performance depends heavily on molding stability, tooling maintenance, coating process control, inspection methods, and traceability.
A capable supplier should be able to explain how it controls:
- Warp and shrink variation in long cosmetic parts
- Surface contamination before painting or lamination
- Coating thickness consistency and cure conditions
- Clip insertion or secondary assembly quality
- Cavity-to-cavity appearance variation
- Packaging protection for class-A surfaces
For technical evaluation, plant audit observations are often more revealing than polished sample boards. Scrap handling, visual inspection lighting, fixture design, rework policy, and defect traceability all indicate whether the supplier can sustain appearance standards over volume production.
Where garnish parts are decorated through in-mold film, painting, vacuum metallization, plating, or hard-coat systems, the evaluator should look closely at process integration. Multi-step cosmetic parts often fail not because any single process is weak, but because process interfaces are poorly managed.
Compliance and specification alignment should be handled carefully
Door garnish does not typically carry the same regulatory burden as lighting or safety-critical systems, but it still sits within broader automotive material, weathering, flammability, chemical, and environmental compliance frameworks. Exact requirements vary by OEM, market, and application. Technical teams should verify applicable material restrictions, surface performance standards, recyclability expectations, and any OEM-specific exterior trim validation requirements.
Where global sourcing is involved, specification drift is a recurring problem. A supplier may quote to a regional material norm while the vehicle program expects an OEM internal standard that is stricter on gloss retention, odor, fogging, or weathering performance. That mismatch often appears late, after tooling or decoration investment has already been made.
If a material claim references compliance, test standards, or restricted substance status without current supporting documentation, it should be marked as 【待核实】 until confirmed through formal documentation review.
How to compare suppliers beyond price and sample appearance
For a robust selection decision, technical evaluators should rank suppliers against the failure risks most relevant to the program rather than scoring everyone against a generic checklist. In practice, the comparison usually becomes clearer when reduced to a few program-specific priorities.
For example:
- If the vehicle is premium and appearance-led, prioritize gloss stability, scratch resistance, and vehicle-level visual harmony.
- If the vehicle is used in harsh climates, prioritize UV durability, thermal cycling stability, and attachment retention after aging.
- If the launch schedule is compressed, prioritize proven tooling discipline, dimensional repeatability, and PPAP readiness.
- If aftermarket service is important, prioritize installation tolerance and field replacement robustness.
This approach is more useful than treating all criteria as equal. Most garnish programs do not fail because every parameter is slightly weak. They fail because one underestimated parameter becomes a visible field issue.
What a sound door garnish selection decision looks like
A sound decision is rarely the part that looks best in a single sample review. It is the part-system-supplier combination most likely to remain acceptable after weathering, assembly variation, logistics, customer cleaning behavior, and multi-market use conditions are applied.
In practical terms, that usually means the preferred solution has:
- A substrate chosen for the true exposure environment, not only initial cost
- An attachment design tolerant of body and process variation
- A finish system aligned with realistic scratch and aging expectations
- Dimensional capability proven over repeated production, not one-off prototypes
- A supplier with visible control over cosmetic manufacturing and packaging risk
For technical evaluators, the most valuable mindset shift is to stop viewing door garnish as decorative trim and start treating it as a high-visibility exterior system component. Once that happens, the right questions become clearer, and supplier differences that seem minor early on become easier to judge before they turn into expensive launch or warranty problems.