
Industry Portal
Related News
- 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions
Precision Forging Explained: Suitable Materials, Tolerances, and Common Limits
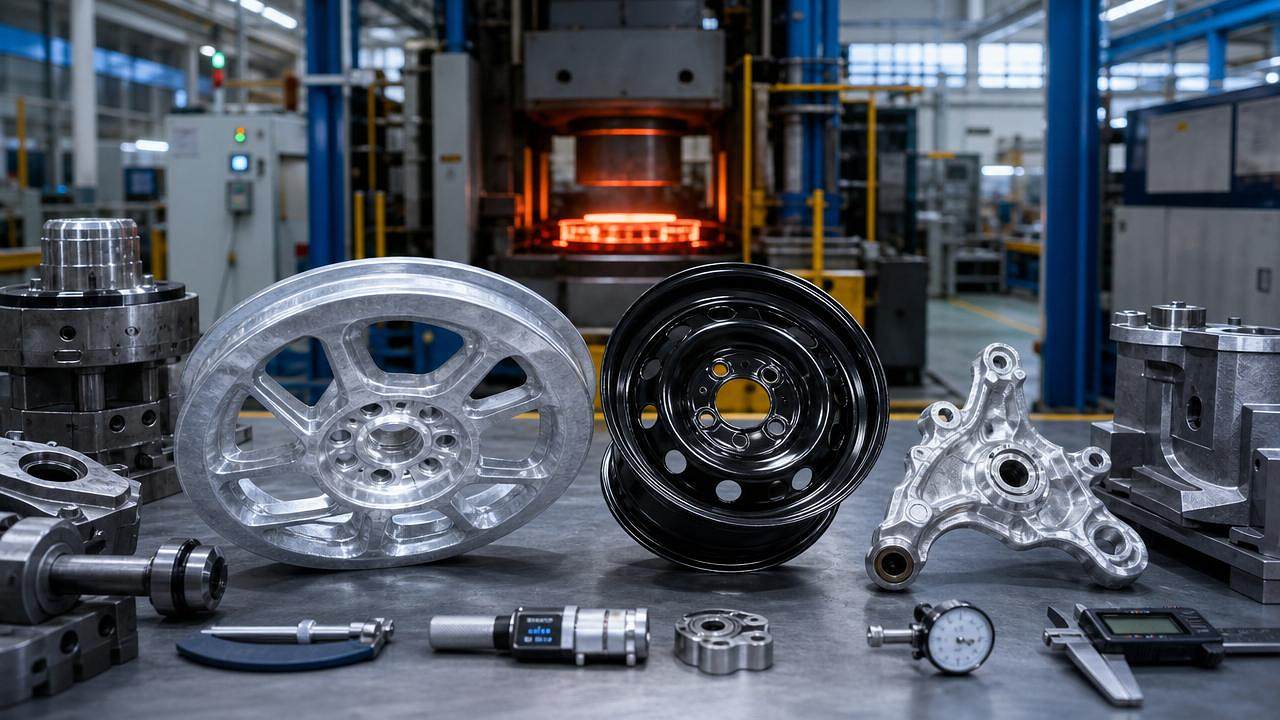
Precision forging sits at the center of many performance-driven automotive decisions. In wheels, suspension links, hubs, and selected structural parts, it shapes how lightweight design, impact resistance, and dimensional stability come together under real operating loads.
That matters even more in the NEV market tracked by AEVS, where exterior efficiency, brake cooling, ride refinement, and safety are tightly connected. A forged part is never only a manufacturing choice. It also affects aerodynamics, durability targets, machining cost, and supply chain risk.
For teams reviewing new programs, the practical questions are usually straightforward: which materials work best, what tolerances are realistic, and where do common process limits begin to change cost or feasibility. Those answers define whether precision forging creates a competitive advantage or becomes an expensive mismatch.
What precision forging really means in production
Precision forging is a near-net-shape forming process that drives heated or warm metal into a controlled die cavity. The goal is to produce geometry close to the final part, reducing downstream machining while preserving a favorable grain flow.
Compared with conventional forging, the emphasis is not only strength. It is also repeatability. The process is designed to deliver tighter dimensions, cleaner surfaces, and better consistency from batch to batch.
In automotive exterior and chassis-related applications, that balance is attractive. A forged wheel blank, for example, can support aggressive lightweighting without giving up impact performance. The same logic applies to steering and suspension components exposed to fatigue and shock.
This is one reason precision forging keeps appearing in AEVS coverage of aluminum alloy wheels and other high-value components. It supports the broader push toward lower mass, tighter quality windows, and premium aftermarket differentiation.
Why the process attracts attention now
The current interest is not only technical. It is commercial. EV platforms carry higher battery weight, stronger instant torque, and stricter expectations for range efficiency. That combination rewards components that are lighter yet stronger.
At the same time, styling pressure has increased. Wheels, visible chassis hardware, and exterior-adjacent parts must fit tighter packaging and cleaner aerodynamic concepts. Precision forging helps when the design intent leaves little room for excess material.
Another driver is compliance. Global programs must account for testing requirements, impact standards, fatigue validation, and traceable process control. A more stable forming route can make qualification easier, especially when production moves across regions or suppliers.
Raw material volatility also matters. When aluminum and alloy costs fluctuate, a near-net-shape process becomes more attractive because unnecessary machining chips and avoidable scrap directly hurt margins.
Suitable materials for precision forging
Material choice depends on more than strength level. Forgeability, thermal behavior, die wear, corrosion needs, and final machining response all influence the decision. In practice, several material groups dominate.
Aluminum alloys
Aluminum is the most visible material in precision forging for lightweight vehicle parts. It is especially common in forged wheels, control arms, knuckles, and brackets where mass reduction directly supports efficiency and ride behavior.
Popular grades often include 6xxx and 7xxx families, depending on the balance between forgeability and final mechanical targets. Aluminum supports attractive strength-to-weight performance, but it demands tight temperature control during forming.
Carbon and alloy steels
Steel remains important where impact toughness, fatigue life, and cost discipline outweigh the need for extreme lightweighting. Precision forging of steel is common in gears, shafts, bearing races, hubs, and heavily loaded connection points.
Steel usually offers a wider mechanical safety margin, but it increases component mass and may require more robust tooling. In mobility programs focused on exterior efficiency, that trade-off should be assessed at system level.
Magnesium and titanium
These materials appear in more selective programs. Magnesium is appealing for extreme weight savings, while titanium serves specialized high-performance or premium use cases. Both can work in precision forging, yet process windows are narrower and costs rise quickly.
For mainstream automotive sourcing, they are usually justified only when packaging, performance, or brand positioning clearly outweighs production complexity.
How tolerances should be understood
Tolerances in precision forging are often discussed too simply. A drawing may show a narrow dimensional band, but achieving it depends on part shape, material flow, die condition, lubricant behavior, and post-forging heat treatment.
Usually, precision forging can hold far better tolerances than open-die or conventional closed-die routes. Even so, the process does not remove the need for finish machining on critical interfaces.
Flatness, roundness, hole position, wall thickness, and flash control should be reviewed separately. A part may look dimensionally stable overall but still drift on a feature that matters for balancing, bearing fit, or assembly alignment.
For forged wheels and rotating parts, tolerance strategy must also include downstream effects. Heat treatment distortion, machining stock allowance, and final runout requirements are often more important than the as-forged number alone.
Typical tolerance influences
- Material temperature variation changes metal flow and final fill.
- Die wear gradually shifts dimensions across production volume.
- Complex ribs and thin sections reduce tolerance stability.
- Heat treatment can distort otherwise accurate forged geometry.
- Inspection strategy determines whether variation is detected early.
Common limits that affect feasibility
Precision forging is powerful, but it has clear limits. The process does not respond well to every shape, every section transition, or every tolerance request. Knowing those boundaries early prevents costly redesign loops.
One common limit is geometry depth relative to material flow path. Deep pockets, sharp corners, and dramatic thickness changes make full die filling harder. That can increase defect risk or force extra machining.
Another limit is feature integration. It is tempting to combine many functions into one forged component, but excessive complexity raises tooling cost, cycle time, and dimensional instability. Near-net-shape is not the same as no-machining.
Part size also matters. Very large forged parts require larger presses, more energy, and more difficult thermal control. Very small precision-forged parts can be feasible, but handling and inspection become disproportionately demanding.
Then there is production volume. Precision forging often makes the most sense when a program can justify die investment through repeat demand, premium performance, or strong scrap reduction versus alternative methods.
Where the business value becomes visible
In many vehicle programs, the value of precision forging appears in system performance rather than in a single purchase price comparison. A lighter wheel can improve acceleration response, brake cooling packaging, and energy use at the same time.
For exterior-related products followed by AEVS, this broader view matters. Aerodynamic wheels, refined NVH behavior, and premium visual quality are often linked to how consistently the base component is formed before finishing.
In the aftermarket, forged wheels show another layer of value. Buyers expect both aesthetics and verified strength. Precision forging supports that expectation when the process route, alloy choice, and testing data are properly aligned.
For global programs, a stable forging route can also reduce launch disruption. Better repeatability helps with PPAP documentation, supplier coordination, and cross-region quality consistency.
Practical checkpoints before locking a route
Early evaluation works best when design, manufacturing, quality, and commercial assumptions are reviewed together. Precision forging decisions tend to fail when one function is optimized in isolation.
- Match alloy selection to actual load case, not only marketing weight targets.
- Separate critical tolerances from nice-to-have drawing preferences.
- Confirm where machining stock is still necessary for fit and balance.
- Check die life assumptions against forecast volume and alloy hardness.
- Review heat treatment distortion and final inspection capability early.
- Compare total conversion cost, not forging price alone.
It is also useful to request evidence from similar parts already in production. A claimed tolerance or weight reduction looks very different when backed by stable CpK data, scrap rates, and field durability history.
A grounded next step
The best use of precision forging starts with a clear map of function, geometry, and allowable process risk. If the component supports vehicle efficiency, visible quality, or high cyclic loading, the process deserves serious review.
From there, material shortlist, tolerance classification, and limit analysis should be built together rather than sequentially. That approach usually reveals whether a forged solution will deliver measurable value or simply move cost downstream.
For organizations tracking lightweight wheels, high-load chassis hardware, and premium exterior performance, the next useful step is to compare candidate parts against real forging capability, validation needs, and raw material exposure before design freeze.