
Industry Portal
Related News
- 00
0000-00
Choosing Low Rolling Resistance Tires for Longer Mileage and Lower Fleet Fuel Costs - 00
0000-00
Rain Sensing Systems Calibration: Methods for Reliable Detection and Testing - 00
0000-00
How to Evaluate a Photoelectric Sensing Supplier for Industrial Automation Projects - 00
0000-00
Automatic Wipers for Buses: 7 Selection Criteria for Fleet Procurement - 00
0000-00
How Smart Optical Perception Prevents Collisions in Low-Light Driving Conditions
EV Wheel Prices: What Buyers Should Compare Beyond the Unit Cost
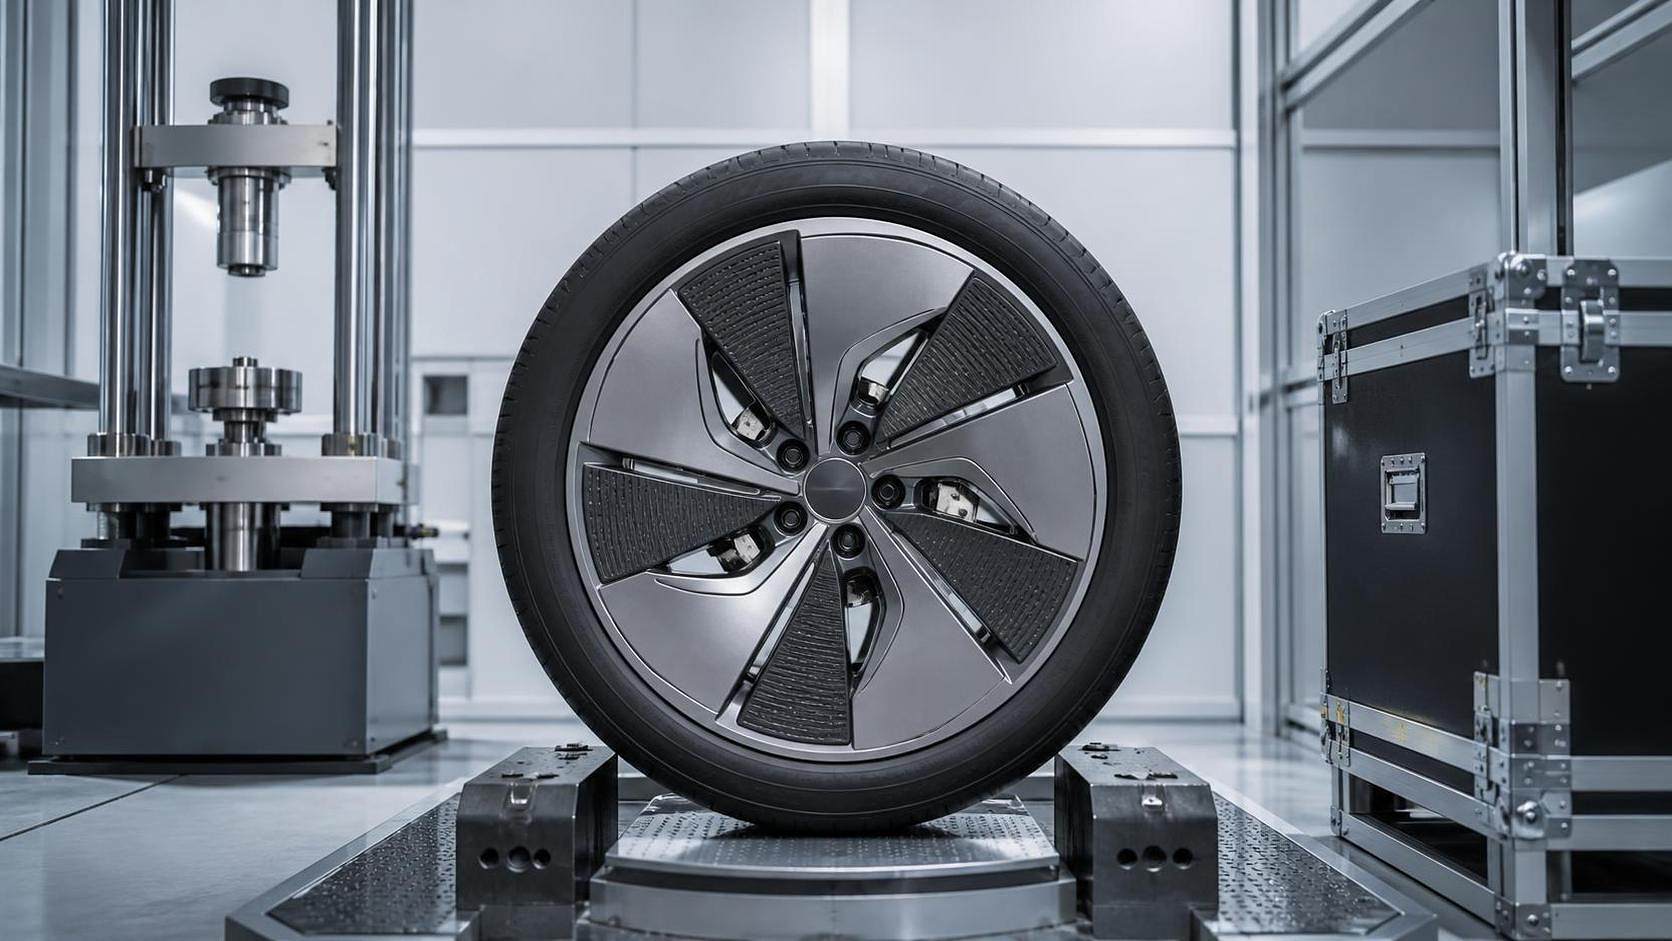
EV wheels price should be treated as an entry figure in a larger technical and commercial comparison. A wheel that appears inexpensive on a quotation can create added cost through higher mass, limited load margin, poor coating durability, difficult replacement matching, or incompatibility with the intended tire and brake package. On an electric vehicle, wheel selection also affects unsprung mass, aerodynamic resistance, rolling behavior, brake airflow, ride response, and the practical service life of adjacent components.
The quoted unit cost therefore needs a defined specification behind it. Diameter, width, offset, bolt pattern, center bore, finish, valve configuration, load rating, and test evidence should all describe the same wheel. A comparison between incomplete quotations rarely identifies the actual lowest-cost option. It only identifies the lowest visible number.
Start With a Comparable Technical Baseline
Before comparing an EV wheels price across sources, establish the vehicle-specific envelope. The nominal wheel size alone is insufficient. A 19-inch wheel, for example, may be produced in different widths, offsets, disc profiles, and barrel geometries. These variations can alter caliper clearance, scrub radius, suspension travel clearance, tire sidewall behavior, and the visual position of the wheel within the arch.
The baseline should include the approved tire size and the vehicle's maximum axle loads. EV battery placement commonly increases curb weight, while fast acceleration can impose substantial longitudinal forces at the tire contact patch. The relevant wheel load requirement should account for the heaviest permitted axle condition rather than an average vehicle mass. A wheel that passes a static calculation with little margin may still be unsuitable when pothole impact, curb contact, payload variation, and dynamic transfer are considered.
Fitment data should be locked before commercial negotiation:
- Nominal diameter and rim width, including the permitted dimensional tolerances.
- Offset, center bore, pitch circle diameter, bolt-seat form, and fastening requirements.
- Required brake caliper and rotor clearance, ideally confirmed through a wheel envelope or physical validation fixture.
- Minimum rated load per wheel, plus the intended validation method for the target application.
- Tire compatibility, including bead-seat contour, recommended rim-width range, and pressure requirements.
- Finish, color standard, center cap arrangement, valve hole design, and any aero cover interface.
Without this baseline, an apparently equal quotation may conceal a narrower rim, reduced material section, a simpler paint process, or a fitment that works only with a different braking system.
Wheel Mass Has a Commercial Effect Beyond Material Consumption
Weight is often discussed as a performance attribute, but it also belongs in cost evaluation. A lighter wheel may reduce the energy needed to accelerate rotating mass and can influence suspension response over uneven surfaces. The real vehicle-level effect depends on tire mass, driving cycle, wheel geometry, and calibration, so range gains should not be assumed from wheel mass alone. Still, excessive mass can create clear engineering compromises, particularly when paired with heavy EV-rated tires.
Mass should be requested per finished wheel, including paint, machining, valve hardware where applicable, and permanently attached trim. Comparing a raw casting weight against a finished forged wheel is not meaningful. It is also useful to request the mass distribution if the design has heavy outer-rim features or attached aerodynamic parts. Material concentrated farther from the hub has a greater effect on rotational inertia than the same mass nearer the center.
A low quoted price can result from a heavier design that uses more material but less sophisticated processing, or from a lighter design with reduced structural reserve. Neither condition is automatically acceptable or unacceptable. The important point is to compare weight together with rated load, test performance, and intended duty cycle. A lightweight wheel with sufficient fatigue and impact margin may justify a different commercial position than a heavy wheel carrying the same nominal dimensions.
Manufacturing Method Changes Both Capability and Risk
Most aluminum alloy EV wheels are supplied as cast, flow-formed, forged, or through related hybrid processes. The method affects grain structure, section design freedom, machining requirements, weight potential, production lead time, and tooling economics. The process description should be specific. Terms such as “forged style,” “performance construction,” or “lightweight alloy” do not identify how the wheel was actually made.
Low-pressure casting can be appropriate for many production applications when process control, heat treatment, X-ray inspection criteria, and machining quality are properly managed. Its economics may suit stable volume programs, although the tooling and approval route need to be accounted for. Gravity casting may have a different cost profile and demands close review of material integrity and process consistency.
Flow forming typically begins with a cast center section and mechanically works the barrel. Depending on the design and process control, this can support reduced barrel thickness and lower weight compared with a conventional cast wheel. It should not be evaluated as equivalent to a fully forged wheel merely because both may be lighter than another cast alternative.
Forging can enable high strength at relatively low mass, but its commercial value depends on the required geometry, machining complexity, finishing steps, and order quantities. A forged wheel with extensive CNC machining, special surface treatment, or a low-volume bespoke fitment can have a substantially different total cost structure from a standard production wheel. Tooling, die life, program changes, and replacement availability deserve attention alongside the invoice price.
Aerodynamics and Brake Cooling Need to Be Assessed Together
Wheel design influences the airflow around the tire, brake assembly, and underbody. On EVs, enclosed or partially covered spoke patterns may reduce turbulence, but an aerodynamic appearance alone does not establish a useful drag outcome. The tire sidewall, wheel-arch geometry, vehicle ride height, rotating spoke surfaces, and attached covers all contribute to the final result.
At the same time, a highly closed face can alter airflow through the brake area. Regenerative braking may reduce friction-brake use in routine operation, yet repeated downhill driving, high payload operation, emergency stops, and brake-conditioning events can still create thermal demand. Brake cooling assessment should reflect the actual brake package and operating conditions rather than assume that reduced routine brake use removes the issue.
Where an aero insert or full wheel cover is used, its retention system becomes part of the wheel decision. The interface should resist vibration, thermal cycling, car-wash exposure, road debris, and repeated removal during tire service. Loose or damaged inserts can create noise, imbalance, appearance claims, and replacement-part complexity. A low-cost cover that requires frequent replacement can quickly erode the apparent advantage of a lower EV wheels price.
Durability Is Defined by the Full Assembly
Wheel durability cannot be separated from tire selection, inflation pressure, vehicle mass, local road condition, and driver use. Low-profile tires may sharpen steering response and enhance appearance, but reduced sidewall height can transfer more impact energy to the wheel. A large-diameter wheel package that looks commercially attractive on paper may create greater exposure to rim damage in applications with poor road surfaces or frequent curb contact.
Validation evidence should identify the exact part number, size, offset, load rating, and finish under review. Generic test reports for a similar wheel family leave room for material differences, revised machining, or changed spoke geometry. Traceability from test sample to serial production is important, especially when a design is altered after initial approval.
Relevant evidence may include radial fatigue, cornering fatigue, impact testing, air-leak evaluation, coating adhesion, corrosion exposure, and dimensional inspection. Test conditions should be matched to the applicable regional requirements and vehicle program criteria. Where regional roadworthiness rules, vehicle regulations, or customer specifications impose particular approval obligations, the required documentation needs to be identified before release rather than after containers are in transit.
Surface finish deserves detailed attention because cosmetic degradation is often treated as a wheel-quality issue even when the structure remains sound. Painted, powder-coated, machined-face, polished, and multi-layer finishes respond differently to stone chipping, brake dust, wheel-cleaning chemicals, salt exposure, and repair attempts. A machined surface beneath clear coat may require a different repair process from a uniform painted wheel. The expected service environment should guide the finish specification.
Unit Price Can Exclude Material Commercial Items
A wheel quotation should state whether it includes tooling, design adaptation, samples, validation parts, center caps, valves, sensors, inserts, packaging, labeling, inspection reports, and export documentation. Freight terms should be equally clear. Wheels occupy substantial volume, and packaging design affects both transport efficiency and finish protection. A compact packaging solution that permits wheel-to-wheel contact may reduce freight cost while increasing cosmetic damage exposure.
For replacement programs, the cost of maintaining a fitment range can exceed the importance of a single wheel's purchase price. Part-number control, finish consistency, batch traceability, minimum order quantities, and the availability of caps or covers after the original production run all affect service cost. Minor shade changes between batches can also matter where a single damaged wheel is replaced rather than a complete set.
Installation Details Can Reveal Hidden Compatibility Costs
A wheel may meet the headline dimensions while creating complications during assembly. Bolt-seat geometry must match the approved fastener design; conical, ball-seat, and flat-seat arrangements are not interchangeable. Incorrect engagement can affect clamp load, centering, and wheel security. Hub-centric location, corrosion at the hub interface, and coating thickness around the center bore should also be considered.
Clearance must be reviewed across full steering lock and suspension travel, not only with the vehicle stationary. Tire growth at speed, snow-chain requirements where relevant, and the position of brake hoses or suspension components can change the usable envelope. For wheels supporting tire-pressure monitoring, the valve and sensor arrangement should be compatible with the specified hardware and service procedure.
Balance quality affects both customer perception and workshop efficiency. Requesting the permitted residual imbalance, the balancing-plane method, and wheel runout limits gives a more useful basis than accepting a general statement of quality control. Excessive corrective weights can be visually unacceptable on open-spoke designs and may indicate issues with wheel geometry, tire matching, or process variation.
Build the Comparison Around Lifecycle Exposure
The most useful commercial comparison connects the wheel's delivered cost to its verified capability and downstream exposure. A lower-cost proposal may be appropriate when it meets the required load, geometry, durability, finish, and documentation criteria without creating additional logistics or service burden. A higher initial cost may also be justified when it reduces wheel mass, supports an aerodynamic target, improves fitment confidence, or offers a more stable replacement path.
Release decisions are strongest when engineering drawings, test evidence, commercial terms, packaging standards, and service-part obligations refer to the same controlled part number. That alignment prevents a common failure mode: a tested sample, an approved drawing, and a delivered wheel that are similar in appearance but not fully identical in specification.
Unit cost remains necessary, but it should sit at the end of a defined comparison rather than at the beginning of one. For EV wheel applications, the wheel is a structural, aerodynamic, thermal, and visual component at once. Its true value emerges only when those roles are measured against the conditions it will face after installation.