
Industry Portal
Related News
- 00
0000-00
How to Specify Low-Pressure Casting Parts for Leak-Tight Automotive Housings - 00
0000-00
How to Specify an Electric Sunroof for Passenger Cars: Key Design and Safety Factors - 00
0000-00
North American Vehicle Aesthetics: Trends Shaping Exterior Design and Materials - 00
0000-00
ASPICE for Smart Optical Systems: Evidence Needed for Automotive Development - 00
0000-00
How to Select NVH Control Materials for Automotive Panels and Powertrain Systems
How Low Pressure Cast Alloy Wheels Are Made and What Affects Their Quality
How Low Pressure Cast Alloy Wheels Are Made and What Affects Their Quality
Low pressure cast alloy wheels sit at the intersection of safety, weight control, cost efficiency, and visual quality.
In modern vehicle programs, they are widely used because they balance structural performance with scalable production.
That balance, however, depends on process discipline.
A wheel may look acceptable on the surface, yet still carry porosity, inclusions, dimensional drift, or heat treatment variation.
For low pressure cast alloy wheels, quality is built in step by step, not inspected in at the end.
This matters even more in EV platforms, where wheel loads rise with battery mass and instant torque.
From a risk and compliance angle, understanding the process is the fastest way to control defects before they reach road use.
What Makes Low Pressure Cast Alloy Wheels Different
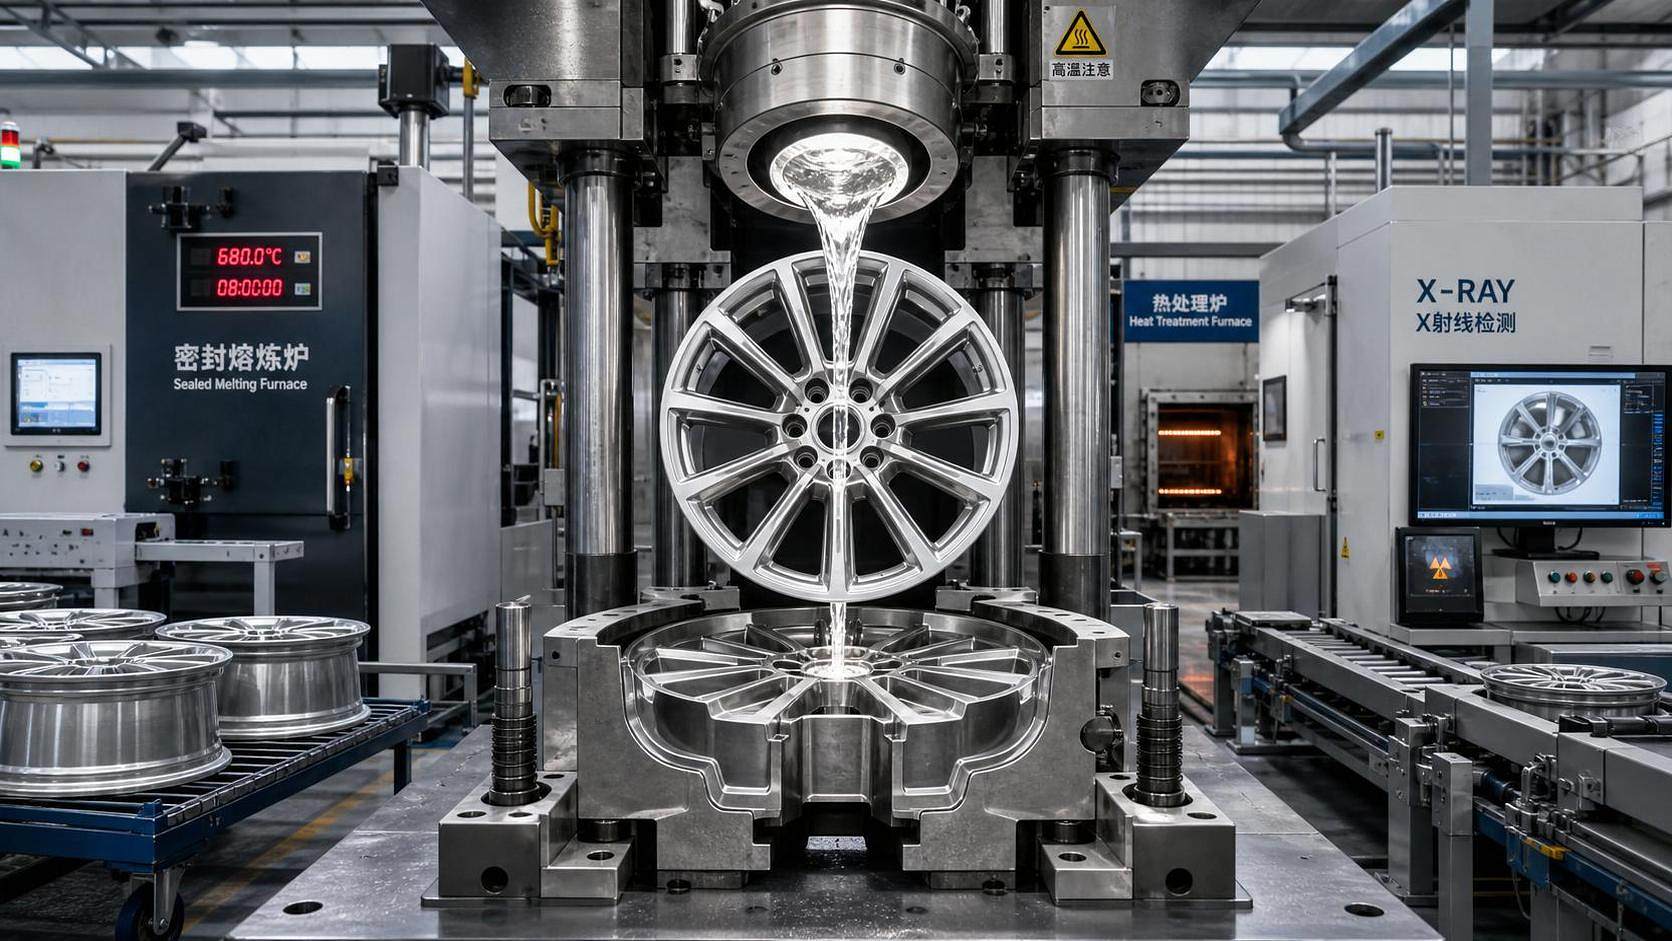
Low pressure casting uses controlled air pressure to push molten aluminum from a sealed furnace into the wheel mold.
The metal rises smoothly through a riser tube, filling the cavity from the bottom upward.
This is one reason low pressure cast alloy wheels usually show better internal soundness than gravity-cast wheels.
The process reduces turbulence, lowers oxide entrainment, and improves feeding during solidification.
It also supports more precise spoke geometry and thinner wall sections.
Still, low pressure cast alloy wheels are only as reliable as the melt, mold, machine settings, and downstream controls behind them.
How Low Pressure Cast Alloy Wheels Are Manufactured
1. Alloy preparation and melt control
The process starts with aluminum alloy selection, often Al-Si-Mg grades such as A356 or equivalent wheel alloys.
Chemistry must stay within a narrow window.
Silicon affects fluidity and shrinkage behavior.
Magnesium supports heat treatment response and final strength.
Before casting, the melt is refined, degassed, and skimmed to reduce hydrogen and non-metallic inclusions.
This early stage has an outsized effect on low pressure cast alloy wheels because internal defects often originate here.
2. Mold preparation
Wheel molds are usually steel and split into sections to form the rim, spokes, hub, and cosmetic features.
Before production, the mold is preheated and coated.
Coating thickness and uniformity affect heat transfer, release behavior, and surface appearance.
Uneven mold temperature can create local solidification differences, which later appear as porosity or dimensional inconsistency.
3. Low pressure filling
Compressed air applies low, controlled pressure inside the holding furnace.
Molten alloy rises into the mold and fills the wheel cavity in a programmed sequence.
Fill speed matters.
Too fast, and turbulence can trap oxides or gas.
Too slow, and the metal may cool early, causing misruns or cold shuts.
For low pressure cast alloy wheels, pressure ramp profiles are usually one of the most tightly managed settings.
4. Solidification and feeding
As the wheel solidifies, pressure is maintained to feed shrinkage and keep the structure dense.
Directional solidification is critical.
The goal is to make metal freeze in a controlled path, avoiding isolated hot spots.
If this control breaks down, low pressure cast alloy wheels can develop shrinkage porosity in spoke roots, hub pads, or rim sections.
5. Demolding, trimming, and heat treatment
After cooling to the target range, the casting is removed and excess material is trimmed.
Most low pressure cast alloy wheels then go through solution treatment, quenching, and artificial aging.
This improves strength, elongation, and fatigue behavior.
Heat treatment is not a routine box to check. It directly shapes the wheel’s mechanical margin.
6. Machining, finishing, and inspection
Critical features are machined after heat treatment.
These include bolt holes, hub bore, bead seats, mounting faces, and balance-related surfaces.
The wheel is then coated, painted, or diamond-cut, depending on design requirements.
Final inspection usually covers dimensions, air leakage, X-ray results, appearance, runout, and mechanical validation.
Key Factors That Affect Wheel Quality
In real production, defects rarely come from one cause alone.
Most low pressure cast alloy wheels fail because several small deviations line up at the same time.
- Melt cleanliness: Hydrogen, oxides, and inclusions remain top drivers of internal rejection.
- Alloy chemistry: Out-of-range composition changes fluidity, strength, and heat treatment response.
- Casting temperature: Excess heat raises gas pickup and grain coarsening; low temperature raises filling risk.
- Pressure curve: Instability during filling or feeding can create porosity and incomplete sections.
- Mold temperature balance: Local overheating or cooling changes shrinkage patterns and cosmetic results.
- Heat treatment consistency: Time, furnace load, and quench delay affect tensile properties and fatigue life.
- Machining accuracy: Poor datum control can cause runout, fit issues, or clamping stress concentration.
- Coating process: Surface contamination or poor curing can hide cracks or weaken corrosion resistance.
From recent manufacturing shifts, the clearer signal is that process variation matters more than isolated nominal settings.
Common Defects in Low Pressure Cast Alloy Wheels
The most common quality risks in low pressure cast alloy wheels are well known, but they still appear in mass production.
For safety-related decisions, defect location matters as much as defect size.
A small pore in a low-stress cosmetic zone is not the same as one near the spoke-to-rim junction.
Inspection and Control Points That Matter Most
A strong control plan for low pressure cast alloy wheels links process inputs to defect modes, then to end-use risk.
- Verify melt chemistry and hydrogen levels by batch, not by assumption.
- Monitor mold temperature maps, not only single-point readings.
- Lock pressure and fill profiles with traceable machine data.
- Use X-ray standards tied to critical wheel sections and acceptance limits.
- Audit heat treatment loads, quench transfer time, and furnace uniformity.
- Check runout, mounting face flatness, and bolt-seat geometry after machining.
- Confirm coating adhesion and corrosion resistance for field durability.
- Correlate inspection data with cornering fatigue, radial fatigue, and impact test outcomes.
This is where standards and technical judgment need to meet.
Depending on market and customer program, validation may reference SAE, JWL, VIA, ECE, or OEM-specific requirements.
Why Quality Expectations Are Rising
The quality bar for low pressure cast alloy wheels is rising for practical reasons, not just paperwork.
EVs bring heavier curb weights, stronger regenerative braking loads, and tighter efficiency targets.
Designs are also becoming more aerodynamic and visually complex.
That means thinner areas, sharper transitions, and less tolerance for hidden casting weakness.
In parallel, global compliance and warranty exposure are making defect escape more expensive than ever.
A Practical Way to Reduce Risk
The most effective approach is simple in principle.
Treat low pressure cast alloy wheels as a controlled system, not a sequence of isolated departments.
Melt control, casting discipline, heat treatment stability, machining precision, and validation feedback must stay connected.
When one step drifts, the next step should detect it quickly.
That is how low pressure cast alloy wheels move from acceptable appearance to dependable road performance.
In daily operations, the strongest results usually come from a short list of stable controls executed consistently.
Focus first on melt cleanliness, pressure profile repeatability, thermal balance, and defect-location-based acceptance. That is where quality becomes measurable, defensible, and safer in service.